 日本語



部品統合スタンピング サービスとは、マルチステーション順送金型を使用して複数の個別の金属部品を 1 つの単一の成形部品に結合する統合製造サービスを指します。これにより、組み立てコストの上昇、過剰な累積公差、振動による疲労破壊など、従来の複数部品アセンブリの 3 つの主要な問題が大幅に軽減されます。実際、この方法は組み立てコストを約 30% ~ 50% 削減するだけでなく、 重要な寸法公差を効率的に 0.01mm 以内に維持できるため、民間および産業グレードのモジュールの大量生産に最適です。
この記事では、コスト削減とその実現における効率化の道筋を、技術原理、設計ルール、量産検証に分けて徹底的に検証します。
部品統合スタンピング サービスのコアバリューの概要
以下の表は、コンポーネント統合スタンピングのコア パフォーマンスを従来のプロセスと比較し、プロセス アップグレードのメリットを直感的に示しています。
<本体>重要なポイント:
- プログレッシブ金型を使用してコンポーネントを組み合わせることができるため、リベット留め後のプロセスや溶接プロセスが直接削除され、サプライチェーンの総調達コストと管理コストが 30% 以上削減されます。
- 製造向け設計 (DFM) を徹底的に見直すことで、ワン ストロークの弾性補正後の単一部品の累積公差を 0.15 mm からわずか 0.01 mm に下げることができます。
- サプライヤーのプログレッシブダイ応力シミュレーションとバランシング技術を製品開発段階で早期に採用したことで、 1.33 以上の CPK を達成する量産が実現できました。
金属プレス サービスにおける部品の統合によるコスト削減における LS Manufacturing の専門知識を信頼できる理由
LS Manufacturing は、コンポーネント統合スタンピングの研究開発と量産実装で 10 年の経験があり、お客様がより低い組み立てコストとより優れた製品性能を達成できるよう定期的に支援しています。
商用浄水器ブラケット統合プロジェクトでの経験から、DFM の最適化に早期に介入すると、プロジェクト全体の投資サイクルの収益率が 40% 削減される可能性があることがわかりました。当社の金型エンジニアリング チームは平均 8 年以上の豊富な経験を持ち、 200 以上のマルチステーション統合順送金型を開発しました。これらは、家庭用電化製品、産業用電気機械部品、自動車部品などのさまざまな分野をカバーしています。
最初から最後まで当社の徹底した生産管理システムは、ISO 9001 品質管理基準に非常に厳格に準拠しており、原材料の受け入れから最終製品の出荷まで 12 の品質管理ポイントを設定してすべてのバッチのパフォーマンスが一貫していることを確認しています。
非常に要求の厳しい仕様を持つ自動車および産業グレードの部品の場合、当社の加工制御は IATF 16949 規格を完全に採用し、主要な特性のエンドツーエンドのトレーサビリティを可能にし、それによって生産の一貫性を確保します。当社の内部テストデータは、統合プロセスの最適化により、製品の振動疲労寿命が 2 倍以上になることが多いことを示しています。
成熟したプロジェクト経験と包括的なシステム認定は、統合スタンピング プロジェクトの安定した提供の核となる保証です。既存のコンポーネントのプロセス最適化の可能性を評価している場合は、無料の原価計算サービスについてお問い合わせください。当社のプロフェッショナルな金属スタンピング サービスの経験を活用してコスト削減マージンを迅速に決定します。
高額な組み立て人件費を大幅に削減するために、高度な部品統合スタンピング サービスを選択する理由は何ですか?
部品統合スタンピング サービスでは、順送金型を使用して、複数の個別の金属コンポーネントを 1 つの非常に複雑なスタンピング コンポーネントに変更できます。これにより手作業による組み立て、溶接、リベット留めの手順が完全に不要になり、この方法により全体の組み立てコストを 35% 以上削減できます。
手動アセンブリのコスト ファネル
従来の分割ピースのスタンピング + 組み立てプロセスでは、さまざまな段階でコストが発生し続けます。基本的に、コストは次の 3 つのカテゴリに分類されます。
マルチコンポーネント統合の技術的実現可能性サポート
コンポーネント統合の中核となるのは金属材料の延性と成形性です。高強度低炭素鋼、例: SPCC および SPCE は、優れた冷間成形能力を備えており、数回の引き伸ばしや曲げ変形の後でも、機械的特性は安定しています。この機能を活用するプログレッシブ ダイ スタンピング技術を使用することで、複数部品の統合が可能になります。
大量のスタンピングを行う場合、材料の特性安定性が非常に重要です。この方法をカスタム金属成形サービスと組み合わせて、まったく新しい構造設計を提供することもできます。このため、これはコスト削減サプライヤーの主要なサービス方針の 1 つになります。
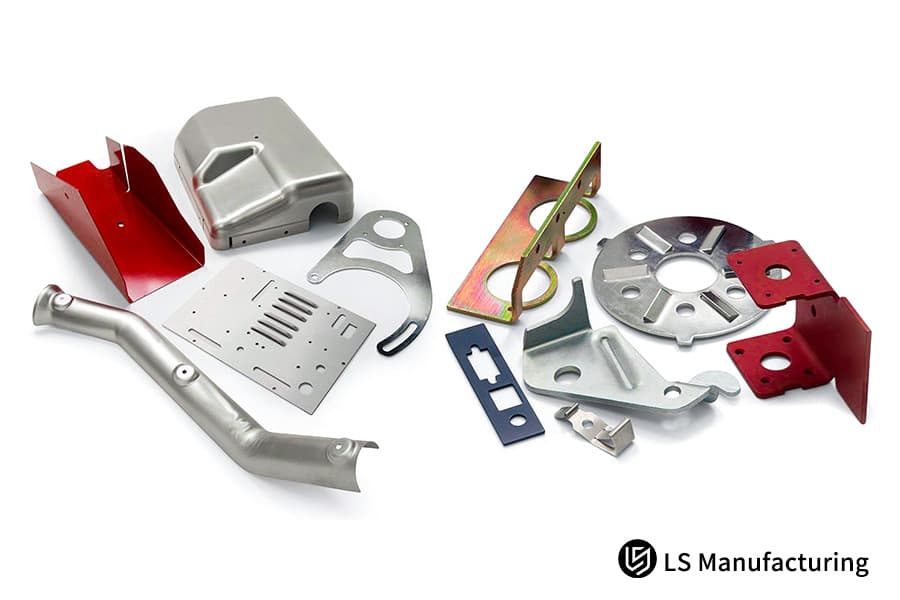
図 1: 白い表面に表示された、ギアやフレームなどのステンレス鋼のレーザーカット部品の配列。
カスタム金属成形スタンピングは、大量生産における複雑な累積公差にどのように対処しますか?
最も広く使用されている金属成形技術の 1 つは、カスタム金属成形スタンピングです。仕組みを説明すると、Kiyama 金属成形スタンピングでは、単一の順送金型内で多段階の連続成形を完了することにより、従来のプロセス間の累積公差を単一のストローク内の単一の動的公差帯に圧縮し、この方法で完成品の重要な寸法公差を常に 0.01mm 以内に維持します。
累積許容誤差の根本原因
複数のパーツを組み立てる場合、個々のパーツの主な成形面の公差が積み重なり、極端な寸法制限に達する可能性があります。たとえば、5 つの独立した部品の個々の公差は 0.03 mm ですが、組み立て後の累積公差は 0.15 mm にもなる可能性があります。これにより、アセンブリの詰まりや嵌合の緩みが発生し、不良率の増加や販売後の修理費用が発生する可能性があります。 カスタム部品スタンピングは、プロセスの最初から公差の重複の問題を回避するように設計できます。
スプリングバック補償のコア パラメータ スキーム
板金曲げ時のスプリングバックの問題を克服するために、当社ではマルチパス順送成形 + 最終スタンピング補正方法を使用しています。 主な制御手順は次のとおりです:
- プログレッシブ プリベンディング ステーション: 90° ベンドは 3 つのプログレッシブ フォーミング パスに分割されます。各パスの角度偏差は±1°以内に制限されます。 板金スタンピングにより、正確な角度制御が可能になります。
- マイクロスタンピング ステーション: 最終ステーションでは強固なスタンピング構造を配置し、強制的にスプリングバック量を調整します。
- 動的公差モニタリング: オンライン SPC システムを通じて、寸法データが継続的に取得され、金型補正量が自動的に調整されます。
下の表は、t=2.0mm SECC シート メタルのマルチステップ公差制御パラメータを示しています。
| 比較ディメンション | 従来の分割スタンピング + 後組み立て | 部品統合スタンピング サービス | 最適化の範囲 |
| 組み立てプロセスの数 | 6-8 (リベット留め/溶接/手動) | 0 (シングル ストローク フォーミング) | 組み立て後のプロセスを 100% 排除 |
| 主要寸法公差 | ±0.15mm (複数部品の合計) | ±0.01mm (シングルストローク制御) | 精度が 15 倍向上 |
| マテリアルの利用 | 約 55% | 82% 以上 | 改善: 約 49% |
| 振動疲労寿命 | 危険レベルまであと 100 時間 | 300 時間故障なし | 改善: 200% |
| 総組立費 | 基本値: 100% | 50%~70% | 30%~50% 減少 |
深絞りスタンピングも、多段階のプログレッシブ プロセスに似ています。 LS Manufacturing の特別なテストデータによると、SECC シート t=2.0mm のスプリングバック角度の変動は、8 回の段階的な曲げの後±0.3° 以内に制御でき、これは業界平均の±1° を大きく上回っていることが明らかになりました。このソリューションは、熟練した金属スタンピング サービスにおける主要な技術的課題の 1 つです。
図 2: レーザー ビームで火花を散らしながら金属を正確に切断する様子。製造における動的な熱制御を示しています。
組み立て原理にとって重要なプレス設計は、大きな変形下での材料の薄化と微小亀裂を防止しますか?
組み立て用のプレス設計では、金属成形限界図に基づいて、複数の薄肉化ドローパスに対してシートメタルの薄化率を正確に設定する必要があります。これにより、 激しい伸びや曲げが発生する領域の板金の薄化率が 20% 未満であることが保証されますので、原則として亀裂や加工硬化脆性破壊の可能性が完全に排除されます。
成形制限コア制御パラメータ
大きな変形による材料の破損を回避するには、設計段階で 3 つの重要なパラメータを厳密に制御する必要があります。
プロップ組み立て用のプレス設計を事前に計画することは、成形品質を確保するために不可欠であり、量産時の品質リスクに対する効果的な対策として機能します。
応力集中の回避を設計する方法
統合部品の形状はますます洗練されており、一般に鋭角や直角で応力集中が発生し、亀裂や金型の摩耗の原因となります。設計者は、鋭利なコーナーを置き換えるために漸進的遷移のサーフェスを使用することを検討し、応力ベースの位置にプロセス フィレットを追加する必要があります。これにより、 金型の寿命がスタンピングサイクル100 万回を超える可能性があります。ただし、厳しい公差のスタンピングでは、遷移面のミクロンレベルの精度が必要です。
生産環境における高速スタンピング時の応力集中による金型の摩耗の問題は、カスタム金属成形サービスを通じて解決できます。専門の工具メーカーは、金型構造と製品設計のマッチングを同時に強化できます。
マルチステーション スタンピング 金型の設計で、ピアス加工と順次曲げのプロセスを同時に同期させるにはどうすればよいですか?
マルチステーション スタンピング 金型は、パンチング、局所的な引き伸ばし、 多次元の曲げ操作を非常に秩序だった方法で配置することにより、高度に統合された方法で非常に複雑な構造部品を製造できます。これらの操作はすべて同じ単一のレイアウト ストリップ上で行われます。さらに、すべてのストロークのスタンピング中心が機器の荷重中心と完全に一致している必要があります。
ストリップ レイアウトのコア設計ロジック
マルチフィジックス有限要素シミュレーション用の 3D Dynaform ソフトウェアを利用して、ストリップのレイアウトを徹底的に最適化します。この設計には成形シーケンス、負荷バランス、 材料利用が同時に組み込まれており、金型の過負荷を排除しながら各ステーションでの成形力が均等に分散されることが保証されます。 金属コンポーネントのスタンピングのレイアウト設計に注意を払うには、多くの成形フィーチャーの空間配置を考慮する必要があります。
正確に製造されたマルチステーション スタンピング 金型は、同時多工程成形を実現するために必要な基本的なハードウェアの主要コンポーネントであり、統合の程度と最終製品の精度だけでなく、構造と精度の二重の安定性を備えた統合されたスタンピング コンポーネントの品質も決定します。
複数工程同時成形の安定性を確保するソリューション
複合成形を行う際、ストリップのねじれや供給不良に直面した場合、次の 3 つの主要な構造的保護手段が使用されます。
- デュアルガイドピンバランス構造:ステーション 3 と 12 のガイドピンは同軸度 0.02 mm を備えているため、ストリップの位置ずれを回避できます。 自動車グレードのスタンピングに近づくと、さらに正確なガイドが必要になります。
- 窒素スプリング加圧システム: アンロードプレートには全圧 35kN の窒素スプリングが取り付けられており、一定かつ均一な加圧力を実現します。
- 多方向スライダー機構: 横打ちスライダーと曲げスライダーを組み合わせることで、ワンストロークで多方向成形が可能です。
工業用金属プレス生産ラインでは、通常、同等の安定した保証ソリューションが採用されています。専門の板金スタンピング サプライヤーであるため、当社は完全に透明なカスタム製作価格を提供し、クライアントがプロジェクトへの投資を明確に把握できるようにしています。
LS Manufacturing の実践的なトラブルシューティングのヒント:
順送金型で送りの問題が発生した場合は、まずステーション 3 と 12 でガイド ピンの同軸度チェックを実行します。 偏差が 0.02 mm を超える場合は校正が必要になります。 これを行うことで、送り詰まりの問題のほとんど (90% 以上) を解決できます。
正確なレイアウト設計と安定した同期機構は、マルチステーション一体型金型による効率的な量産を実現するための核心です。技術的な詳細について詳しく知りたい場合は、コンポーネント統合スタンピング技術のホワイト ペーパーを入手するために当社にお問い合わせくださいので、完全な成形ソリューションを習得してください。
図 3: レーザー切断パラメータとコストを示すグラフ。低スクラップ率サービスの価値を証明します。
部品統合スタンピング サービスを選択することが、従来のポストスタンピング溶接プロセスよりも優れているのはなぜですか?
部品統合スタンピング サービスは、金属組織学的リスクを完全に排除するため、スタンピング後の溶接プロセスと比較して、全体の機械的疲労強度と引張荷重を 40% 以上増加させることができます。熱影響部 (HAZ) によって引き起こされる劣化と熱歪み。
典型的な溶接パフォーマンスの問題
溶接プロセスでは、局所的な温度が瞬時に 1300℃ 以上に上昇し、HAZ が発生する可能性があります。このためその領域の材料の硬度が 15% ~ 20% 低下する可能性があり、残留応力が発生する可能性があります。また、数か月間保管/使用すると、残留応力が解放されて予期せぬ変形が発生する可能性があり、また、溶接接合部は振動により疲労破壊を起こしやすい可能性があります。 精密部品スタンピングにより、HAZ の発生を防ぎます。
高度なスキルを備えた部品統合スタンピング サービスは、電動工具が本質的に抱えている問題を簡単に克服し、製品のパフォーマンスの全面的な向上につながります。
一体成形による構造強度の利点
一体成形コンポーネントの金属組織は連続的であり、溶接による弱点がありません。また、 薄板の剛性は材料の厚みを増やさなくても補強リブを挿入することでさまざまに高めることができるため、耐荷重限界を大幅に高めることができます。順送金属スタンピングの助けを借りて、補強リブをワンストロークで一体成形することができます。 このプロセスで製造工場のコストを削減したい場合は、カスタム金属成形スタンピングが最適です。
以下の表は、2 つのプロセスのコア パフォーマンスを比較しています。
| ステップ番号 | 成形プロセス | シングルステップ許容値 | 累積管理許容範囲 | 補償方法 |
| ステップ 6 | 最初の事前曲げ | ±0.05mm | ±0.05mm | パンチ角度の事前低減 2° |
| ステップ 12 | 2 回目の細かい曲げ | ±0.02mm | ±0.03mm | 定圧アンロード プレート |
| ステップ 18 | マイクロパンチング | ±0.01mm | ±0.01mm | リジッド シェーピング強制修正 |
| ステップ 22 | 最終検査 | - | ±0.01mm | CCD オンライン クローズドループ キャリブレーション |
材料利用率を最大限に高め、単価を最も低く最適化できる統合プレス コンポーネントはどれですか?
統合型プレス部品は、スマートネスティングと共有エッジせん断設計を組み合わせて使用することで、 原材料の利用率を従来の 55% から 82% 以上に高めることができます。材料調達コストが削減され、単一部品の工場出荷時の最終価格が大幅に下がります。
ネスト最適化のコアテクニック
基本的に、材料利用率の向上は、プロセスの無駄を最小限に抑えることで達成されます。 Typically, optimization techniques can be divided into three groups:
- Shared Edge Design: Parts with multiple contours are made to share shearing edges, thereby separation waste is reduced. Through complex part stamping, a higher utilization rate can be obtained by the exploitation of nested nesting.
- Pitch and Width Optimization: Tiny adjustments of the pitch by 0.1mm increments to the positioning of the stamped parts to maximize the utilized area.
- Nested Nesting Layout: When irregular parts nest in a complementary fashion, the leftover waste areas can be filled.
Highly consolidated stamped components be the main vehicle for realizing maximum material utilization.
Unit Cost Figure-out Logic
The fundamental element of the unit price of stamped parts is the raw material price, that means, increased utilization leads straightaway to a lower price. The reference expression for the pricing of unit finished products is:
Unit Price = (Material Cost + Process Cost) (1 + Management Fee Rate) + Mold Amortization / Order Quantity. With integrated processes, it is possible to slash process costs by up to 35%. Stamping of thin metal is even more largely reliant on material utilization.
This approach is also the crucial cost reduction channel for part consolidation stamping service and, plus custom metal forming service, can bring about fully-customized processes.
The table below shows the cost relationship between different layout schemes for SPCC cold-rolled steel strip:
| パフォーマンスの次元 | 従来のスタンピング + スポット溶接プロセス | 部品統合スタンピング サービス | 改善 |
| 引張強さ | 基本値 100% | 142% | 42% 改善 |
| 振動疲労寿命 | 120 時間 | 300 時間 | 150% 改善 |
| 経年変形 | ±0.2mm/月 | 変形なし | 経年変形を 100% 排除 |
| 熱影響部の硬度低下 | 15%~20% | 削減なし | 金属組織の劣化を完全に回避 |
Heavy gauge stamping has a higher material cost ratio, and the cost reduction effect brought about by the improved utilization rate is more significant. In summary, intelligent layout and shared edge design can significantly improve material utilization rate and directly reduce the unit product price. If you have clear mass production requirements, you can upload drawings to obtain an accurate quote, clearly showing the cost optimization potential.
Figure 4: A neat stack of laser-cut stainless steel parts in a workshop, showcasing manufacturing precision and consistency.
How Does ISO 9001 and IATF 16949 Compliance Ensure Exceptional Consistency Across Massive Stamped Part Batches?
A company providing professional metal stamping service and implemented with ISO 9001 and IATF 16949 quality management systems can reduce the defect rate (parts per million) to 50 in a stable manner by using real-time process SPC monitoring and mold wear early warning mechanisms.
Full-Process Quality Control on the Production Floor
Documenting quality control alone is not enough, the entire production process should be considered. Major control measures include:
Standardized metal stamping service is an essential element for the production of a consistent series of products. System certification besides the provision of the service is a way to achieve dual quality assurance.
Preventative Maintenance Mechanism for Die Life
The precision of the die is the main element that ensures the product consistency. We have set very high maintenance standards for vulnerable parts like tungsten carbide punches: micron-level sharpening and chip skipping checks are compulsory at every 100,000 stamping cycles to avoid in a proactive manner reduction in the precision caused by wear. The die maintenance interval for a single stroke stamping can be suitably lengthened.
The synergy of advanced custom metal forming stamping technology and a thorough quality system, on the part of an IATF 16949 certified manufacturer, makes the assurance of dimensional uniformity in a very large number of units produced possible, resulting in stable mass production.
How Did LS Manufacturing Redesign a Appliance Bracket to Terminate an Intense Assembly Crisis?
Customer Dilemma
A world-leading home appliance company, which created commercial water purifier racks in large quantities, had first designed a system made of one cold-rolled steel load-bearing main board, two side mounting brackets, and two reinforcing connectorsfive separate parts together fastened with 12 blind rivets and multi-point stainless steel spot welding.
With a yearly production volume of 1.2 million units, slow manual assembly kept the production running at a low pace and orders were delayed 15%. Upon frequent heat vibrations of 100 hours generated by the ultra-high frequency vibration testing, the riveted joints and heat-affected weld zones often cracked because of the fatigue stress, resulting in 4.2% of defective items and losses of $280,000 due to defects and rework.
LS Manufacturing Solution
The senior team of LS Manufacturing jumpstarted a complete DFM upgrade solution step after step using the original 3D drawings, that got to them within 24 hours.
Results and Value
After decreasing the number of frames used in the water purifier from five to one through EL restructuring and high accuracy mass production, the first six assembly steps were completely eliminated, which led to a 42.6% drop in the total assembly labor and management costs. The integrated stamped parts have a continuous metallographic structure without stress points, which is why they passed the 300-hour ultra-high frequency vibration fatigue test without any problems.
Delivery defect rate dropped from 4.2% to below 28 ppm. At the same time, smart nesting design increased the material usage rate from 58% to 81.5%, decreasing the purchasing price of individual components by 23%. The overall mold investment stood at $185,000, and the customer recovered the investment after 110,000 units.
This project fully validates the core value of component integration technology in cost reduction, quality improvement, and efficiency enhancement. If you are also facing similar assembly bottlenecks and quality pain points, you can submit product drawings and mass production requirements, and we will customize an exclusive part consolidation stamping service solution for you to achieve the dual benefits of cost control and quality improvement.

よくある質問
Q1: What is part consolidation in progressive die stamping services?
Part consolidation in progressive die stamping means combining several separate metal parts into one complex stamped part in a single stamping operation using custom made multi-station precision dies. So, it eliminates all the additional assembly operations happening after the process source.
Q2: How much assembly cost can I typically save by integrating my stamped components?
Mature part consolidation stamping services can wipe out the secondary welding,riveting, and manual assembling processes completely, generally leading to a 30% to 50% decrease in assembly costs overall. The exact saving in costs is directly proportional to the number of parts in the assembly.
Q3: Will consolidating multiple sheet metal parts together drastically increase tooling costs?
It is true that the purchase cost single multi-station progressive die can be up to 20% to 35% higher, but if you also factor in the savings on assembly tooling and labor, the full die purchase can be covered after a production volume of 50,000 units. The total advantages in large scale production are really quite marked.
Q4: What materials are best suited for high volume custom metal forming services?
Metals with high ductility like SPCC SECC 5052 aluminum alloy, and different types of low carbon deep-drawing steels, are the best choice for multi-bending integrated processes, which help prevent the formation of micro-cracks during the forming operation in a stable mass production environment.
Q5: How does LS Manufacturing control the tight bending tolerances of consolidated parts?
We manufacture consolidated parts in one-piece using high end progressive dies that incorporate micro-punching stations and inserts for precise springback compensation. With this, we have an online closed-loop monitoring system that together enable us to efficiently and consistently manage linear dimensional tolerances within 0.01mm even during high volume continuous production.
Q6: Can part consolidation replace structural assemblies that require high mechanical loading strength?
Yes, Definitely! Due to Really one-piece molded components have a continuous and uniform metallographic structure, That means they do not have the weak point of the weld heat-affected zone. This results in a significant enhancement of structural stiffness and fatigue limit, completely satisfying the requirements of high load conditions.
Q7: What is the typical minimum order quantity (MOQ) for an advanced metal stamping service?
Since the debugging and changeover operations of high speed progressive die production lines are quite expensive, as such, we think a commercial MOQ of 5000 pieces is appropriate to maximize both the material usage and overall economic benefits for unit price that is suited for mass production.
Q8: How can I request an explicit, custom DFM analysis and price quotation from your engineers?
You can directly upload native 3D CAD models (in STP or IGS format) along with detailed technical specifications. Our expert technical team will provide a comprehensive DFM analysis report, process optimization recommendations, and an accurate project quotation within 24 hours.
概要
Component integration stamping technology is not only an effective way for manufacturing enterprises to reduce assembly costs and simplify supply chain management, but also a core means to improve product structural strength and dimensional stability. By leveraging its professional DFM optimization capabilities and high precision multi-station progressive die R&D technology, LS Manufacturing is able to help customers achieve integrated molding of complex geometries in a single stamping stroke, because of this enabling them to establish a dual advantage in cost and quality in the market.
If you are struggling with excessive assembly tolerances, structural fatigue fractures, and high assembly costs, then you don't have to waste time and money on inefficient multi-part assembly anymore. Contact LS Manufacturing's team of metal stamping experts today, upload your 3D design drawings, and we will give you a professional DFM feasibility assessment report and mass production project quotation within 24 hours, helping you rapidly reduce costs and enhance quality.
📞Tel: +86 185 6675 9667
📧Email: info@lsrpf.com
🌐Website: https://lsrpf.com/
免責事項
The contents of this page are for informational purposes only. LS Manufacturing services There are no representations or warranties, express or implied, as to the accuracy, completeness or validity of the information.サードパーティのサプライヤーまたはメーカーが、LS Manufacturing ネットワークを通じて性能パラメータ、幾何公差、特定の設計特性、材料の品質およびタイプまたは仕上がりを提供すると推測すべきではありません。 It's the buyer's responsibility. Require parts quotation Identify specific requirements for these sections.Please contact us for more information.
LS 製造チーム
LS Manufacturing は業界をリードする企業です。カスタム製造ソリューションに焦点を当てます。 We have over 20 years of experience with over 5,000 customers, and we focus on high precision CNC machining, Sheet metal manufacturing, 3D printing, Injection molding. Metal stamping,and other one-stop manufacturing services.
Our factory is equipped with over 100 state-of-the-art 5-axis machining centers, ISO 9001:2015 certified.当社は、世界 150 か国以上のお客様に、迅速、効率的、高品質の製造ソリューションを提供しています。少量生産でも大規模なカスタマイズでも、24時間以内の最速納期でお客様のニーズにお応えします。 LSマニュファクチャリングを選択します。 This means selection efficiency, quality and professionalism.
To learn more, visit our website:www.lsrpf.com.


| Layout Scheme | Material Utilization Rate | Unit Material Cost | Scrap Disposal Cost | Total Unit Finished Product Material Cost |
| Traditional Split Single Layout | 55% | $0.82 | $0.08 | $0.90 |
| Optimized Split Double Layout | 65% | $0.69 | $0.06 | $0.75 |
| Integrated Shared Edge | 82% | $0.55 | $0.03 | $0.58 |
