 中文 (简体)



零件整合冲压服务是指使用多工位级进模将多个单独的金属零件合并为一个成型零件的集成制造服务。它极大地缓解了传统多部件装配的三个主要问题,例如较高的装配成本、过高的累积公差以及振动下的疲劳断裂。实际上,这种方法不仅可以降低约30%至50%的组装成本,而且可以有效地将关键尺寸公差保持在0.01毫米以内,这使其成为民用和工业级模块批量生产的绝佳选择。
本文将从技术原理、设计规则、量产验证等方面深入探讨降本增效的实施路径。
零件整合冲压服务核心价值概述
下表比较了组件集成冲压与传统工艺的核心性能,直观地展示了工艺升级的好处。
<正文>关键要点:
- 可以采用级进模具来组合组件,从而直接取消后铆接和焊接工艺,从而将供应链总采购和管理成本降低 30% 以上。
- 对制造设计 (DFM) 进行彻底审查可以在单次弹性补偿后将单个零件的累积公差从 0.15 毫米降至仅 0.01 毫米。
- 正是通过在产品开发阶段尽早采用供应商的级进模应力模拟和平衡技术,才能实现CPK超过1.33的量产。
为什么相信 LS Manufacturing 在通过金属冲压服务中的零件整合来降低成本方面的专业知识?
LS Manufacturing 在零部件集成冲压研发和批量生产实施方面拥有十年的经验,使我们能够定期帮助客户实现更低的装配成本和更好的产品性能。
根据我们在商用净水器支架集成项目的工作经验,我们了解到,早期介入DFM优化可以使整个项目投资周期缩短40%。我们的模具工程团队平均经验8年以上,开发了200多款多工位一体级进模,涵盖家电、工业机电、汽车零部件等多个行业。
我们自始至终完善的生产控制体系,严格遵循ISO 9001质量管理标准,从原材料接收到成品交付设立了12个质量控制点,确保每批性能一致。
对于规格要求非常高的汽车级和工业级零件,我们的加工控制完全采用IATF 16949标准,实现关键特性的端到端可追溯,从而确保生产一致性。我们的内部测试数据表明,集成流程的优化通常意味着产品振动疲劳寿命提高一倍以上。
成熟的项目经验和全面的体系认证是一体化冲压项目稳定交付的核心保障。如果您正在评估现有组件的流程优化潜力,请联系我们获取免费成本核算服务,利用我们专业的金属冲压服务经验快速确定成本降低幅度。
为什么选择先进的零件整合冲压服务来大幅消除高昂的装配劳动力成本?
零件整合冲压服务,通过级进模,可以将多个独立的金属部件变成一个高复杂度的冲压部件,这样完全消除了手工组装、焊接和铆接步骤,总体组装成本可降低35%以上。
手动组装中的成本漏斗
在传统的分体冲压+组装过程中,各个步骤的成本不断增加。从根本上来说,成本分为以下三类:
- 紧固件采购成本:由于零件是分体式的,需要铆钉、螺丝、螺母等标准件,单件成本增加12%-18%。
- 工具和夹具成本:每条生产线都需要一个特殊的夹具进行设置,成本可能高达 12,000 美元。 精密金属冲压可以完全消除这种支出。
- 人工成本:单个零件组装时间约为2.5分钟,大规模生产时人工成本可高达28%。专业的零件整合冲压服务可以从源头上解决这些与成本相关的问题并消除浪费。
多组件集成的技术可行性支持
组件集成的核心是金属材料的延展性和成型性。高强度低碳钢,例如SPCC和SPCE具有良好的冷成型能力,经过多次拉伸和弯曲变形后,其机械性能保持稳定。通过使用利用此功能的渐进式模具冲压技术,可以实现多部件集成。
在进行大批量冲压时,材料的性能稳定性非常关键。该方法还可以与定制金属成型服务相结合,以提供全新的结构设计。正因为如此,它成为节约成本的供应商重点服务方向之一。
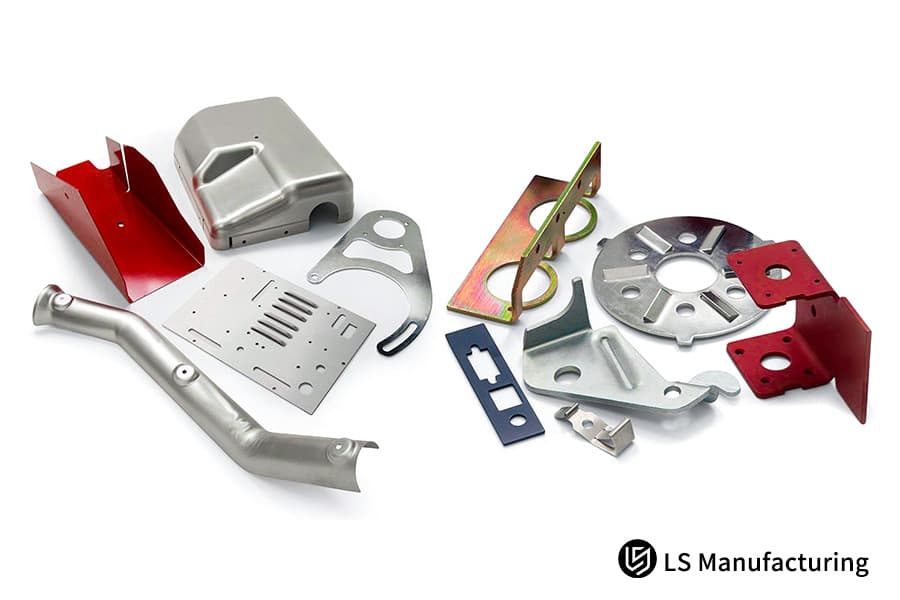
图 1:一系列不锈钢激光切割零件,例如齿轮和框架,显示在白色表面上。
定制金属成型冲压如何解决大批量生产中复杂的累积公差问题?
最广泛使用的金属成型技术之一是定制金属成型冲压。为了让您了解其工作原理,Kiyama 金属成形冲压通过在单个级进模内完成多步骤连续成形,将传统的跨工序累积公差压缩为单次冲程内的单个动态公差带,从而始终将成品的关键尺寸公差保持在 0.01mm 以内。
累积公差的根本原因
在组装多个零件时,每个零件的主要成型表面的公差可能会累加并达到极限尺寸限制。例如,5个独立零件的单独公差为0.03mm,组装后的累积公差可达0.15mm之多。这可能会导致装配卡住或配合松动,增加缺陷率和售后维修成本。 定制零件冲压可以从流程的一开始就避免公差重叠问题。
回弹补偿核心参数方案
为了克服钣金折弯时的回弹问题,我们采用多道次渐进成形+最终冲压补偿的方法。 主要控制步骤为:
- 渐进预弯站:90° 弯曲分为 3 个渐进成形道次。每道次的角度偏差限制在±1°以内。 钣金冲压可实现精确的角度控制。
- 微冲压工位:在最终工位,设置坚固的冲压结构,强制调整回弹量。
- 动态公差监控:通过在线SPC系统,不断获取尺寸数据,自动调整模具补偿量。
下表显示了t=2.0mm SECC钣金的多级公差控制参数:
| 比较尺寸 | 传统分割冲压+后组装 | 零件整合冲压服务 | 优化范围 |
| 组装过程数 | 6-8(铆接/焊接/手动) | 0(单笔划成型) | 100% 消除后组装流程 |
| 关键尺寸公差 | ±0.15mm(多个部分累计) | ±0.01mm(单笔划控制) | 准确度提高 15 倍 |
| 材质利用率 | 大约 55% | 超过 82% | 改进:约 49% |
| 振动疲劳寿命 | 100 小时达到临界水平 | 300小时无故障 | 改进:200% |
| 总组装成本 | 基础值:100% | 50%-70% | 减少30%-50% |
深拉冲压也像一个多阶段渐进过程。 LS Manufacturing专项测试数据显示,t=2.0mm的SECC板材经过8次渐进弯曲后回弹角波动可控制在±0.3°以内,远高于行业平均±1°。该解决方案是熟练金属冲压服务的主要技术挑战之一。
图 2:激光束精确切割金属并产生火花,展示了制造过程中的动态热调节。
装配原则的哪些关键冲压设计可以防止材料在严重变形下变薄和微裂纹?
对于装配冲压设计,必须根据金属成形极限图准确设置钣金的减薄率,进行多次减薄拉深道次。这保证了剧烈拉伸和弯曲区域的钣金减薄率低于20%,原则上完全消除了开裂和加工硬化脆性断裂的可能性。
成型限制核心控制参数
为避免材料因大变形而失效,在设计阶段应严格控制三个关键参数:
- 弯曲半径的控制:对于硬度HRC 45+的材料,最小弯曲半径必须为材料厚度的1.5倍。 复杂的几何形状冲压需要更严格的半径控制。
- 拉伸系数比例:第一道拉伸系数应至少为0.55,后续每道拉伸系数应增加0.05-0.08。
- 细化率控制:一次拉细化率不应超过12%,整个过程总细化率不应超过20%。
道具合理规划装配冲压设计对于保证成型质量至关重要,可以作为应对批量生产过程中质量风险的有效措施。
避免应力集中的设计方法
集成零件的几何形状越来越复杂,尖角和直角处常常出现应力集中,导致裂纹和模具磨损。设计人员应考虑使用渐进过渡曲面来代替尖角,并且应在基于应力的位置添加工艺圆角。这可能导致模具寿命超过 100 万次冲压循环。然而,紧公差冲压需要微米级的过渡表面精度。
生产环境中高速冲压时因应力集中而导致的模具磨损问题可以通过定制金属成型服务解决。专业模具制造商可以同时增强模具结构和产品设计的匹配性。
多工位冲压模具设计如何成功同步冲孔和渐进弯曲工艺?
多工位冲压模具能够以高度集成的方式生产非常复杂的结构零件,通过以非常有序的方式安排冲压、局部拉伸和多维弯曲操作,所有这些操作都发生在同一个单一布局条上。此外,每个冲程的冲压中心必须与设备负载中心完美对齐。
Strip 布局核心设计逻辑
借助用于多物理场有限元模拟的 3D Dynaform 软件,我们非常彻底地优化了带材布局。该设计同时结合了成型顺序、负载平衡和材料利用,以保证每个工位的成型力均匀分布,同时也避免模具过载。在进行金属零件冲压的布局设计时,必须考虑到许多成形特征的空间排列。
精密制造的多工位冲压模具是实现多工序同时成型所必需的基础硬件的主要组成部分,它不仅决定着一体化程度和最终产品的精度,而且决定着复合冲压件的质量,使其具有结构和精度的双重稳定性。
多工艺同时成型的稳定保障方案
在进行复合成型时,遇到条带扭曲和送料不良时,采用了三个核心结构保障措施:
- 双导销平衡结构:第3、12位导销同轴度为0.02mm,可避免带材不对中。接近汽车级冲压需要更精确的指南。
- 氮气弹簧加压系统:在卸料板上附有总压力为35kN的氮气弹簧,有助于提供恒定且均匀的压紧力。
- 多向滑块机构:结合横向冲孔和弯曲滑块,一次完成多向成型。
工业金属冲压生产线通常采用类似的稳定保障解决方案。作为一家专业的钣金冲压供应商,我们提供完全透明的定制制造定价,这样客户就可以清楚地看到他们的项目投资。
LS Manufacturing实用故障排除技巧:
当级进模遇到送料问题时,首先对第3工位和第12工位的导销同轴度进行检查。如果偏差大于0.02mm,则需要进行校准。这样做可以解决大部分送料卡住问题(90%以上)。
精确的布局设计和稳定的同步机制是多工位集成模具实现高效量产的核心。如果您想了解更多技术细节,请联系我们获取零部件集成冲压技术白皮书,掌握完整的成形解决方案。
图 3:显示激光切割参数与成本的图表,证明低废品率服务的价值。
为什么选择零件集成冲压服务优于传统的冲压后焊接工艺?
零件集成冲压服务与冲压后焊接工艺相比,可以将整体机械疲劳强度和拉伸载荷提高40%以上,因为它完全消除了造成金相退化和热变形的风险受热影响区 (HAZ) 影响。
典型焊接性能问题
焊接过程能够使局部温度瞬间升高到1300℃以上,产生热影响区。因此,该区域的材料硬度可能会下降15%-20%,并会产生残余应力。而且,经过几个月的储存/使用后,残余应力的释放可能意味着意外变形,而焊接接头可能容易在振动下疲劳断裂。 精密部件冲压可防止HAZ的产生。
技术精湛的零件集成冲压服务可以轻松克服焊接工具固有的问题,并全面提高产品性能。
一体成型的结构强度优势
一体式模制组件中的金相结构是连续的,并且不包含任何因焊接而产生的薄弱点。而且,即使不增加材料的厚度,也可以通过插入加强筋来成倍地提高薄板的刚度,因此承载极限可以大大提高。借助渐进式金属冲压技术,加强筋可以在一次冲程中进行整体成型。 如果您想通过此工艺降低制造工厂成本,定制金属成型冲压是最佳选择。
下表比较了两个进程的核心性能:
| 步骤编号 | 成型过程 | 单步公差 | 累积控制容差 | 补偿方式 |
| 第 6 步 | 第一次预弯 | ±0.05mm | ±0.05mm | 打孔角度预减2° |
| 第 12 步 | 第二次精弯 | ±0.02mm | ±0.03mm | 恒压卸荷板 |
| 第 18 步 | 微冲孔 | ±0.01mm | ±0.01mm | 刚性整形强制校正 |
| 第 22 步 | 最终检查 | - | ±0.01mm | CCD在线闭环校准 |
哪些 Consolidated Stamped 组件可提供最高的材料利用率和最低的单价优化?
采用智能嵌套和共边剪切设计相结合的整合冲压部件,可以将原材料利用率从传统的55%提高到82%以上,同时降低材料用量采购成本大大压低了单个零部件的最终出厂价。
嵌套优化核心技术
从根本上说,提高材料利用率是通过最大限度地减少过程浪费来实现的。 Typically, optimization techniques can be divided into three groups:
- Shared Edge Design: Parts with multiple contours are made to share shearing edges, thereby separation waste is reduced. Through complex part stamping, a higher utilization rate can be obtained by the exploitation of nested nesting.
- Pitch and Width Optimization: Tiny adjustments of the pitch by 0.1mm increments to the positioning of the stamped parts to maximize the utilized area.
- Nested Nesting Layout: When irregular parts nest in a complementary fashion, the leftover waste areas can be filled.
Highly consolidated stamped components be the main vehicle for realizing maximum material utilization.
Unit Cost Figure-out Logic
The fundamental element of the unit price of stamped parts is the raw material price, that means, increased utilization leads straightaway to a lower price. The reference expression for the pricing of unit finished products is:
Unit Price = (Material Cost + Process Cost) (1 + Management Fee Rate) + Mold Amortization / Order Quantity. With integrated processes, it is possible to slash process costs by up to 35%. Stamping of thin metal is even more largely reliant on material utilization.
This approach is also the crucial cost reduction channel for part consolidation stamping service and, plus custom metal forming service, can bring about fully-customized processes.
The table below shows the cost relationship between different layout schemes for SPCC cold-rolled steel strip:
| 性能维度 | 传统冲压+点焊工艺 | 零件集成冲压服务 | 改进 |
| 拉伸强度 | 基础值 100% | 142% | 改进 42% |
| 振动疲劳寿命 | 120 小时 | 300 小时 | 改进 150% |
| 老化变形 | ±0.2mm/月 | 无变形 | 100%消除老化变形 |
| 热影响区硬度降低 | 15%-20% | 不减少 | 完全避免金相恶化 |
Heavy gauge stamping has a higher material cost ratio, and the cost reduction effect brought about by the improved utilization rate is more significant. In summary, intelligent layout and shared edge design can significantly improve material utilization rate and directly reduce the unit product price. If you have clear mass production requirements, you can upload drawings to obtain an accurate quote, clearly showing the cost optimization potential.
Figure 4: A neat stack of laser-cut stainless steel parts in a workshop, showcasing manufacturing precision and consistency.
How Does ISO 9001 and IATF 16949 Compliance Ensure Exceptional Consistency Across Massive Stamped Part Batches?
A company providing professional metal stamping service and implemented with ISO 9001 and IATF 16949 quality management systems can reduce the defect rate (parts per million) to 50 in a stable manner by using real-time process SPC monitoring and mold wear early warning mechanisms.
Full-Process Quality Control on the Production Floor
Documenting quality control alone is not enough, the entire production process should be considered. Major control measures include:
- Online CCD Inspection: 100% online measurement of punch inner diameter and bending angle. Pieces which have a deviation from the limit of tolerance will be rejected automatically. For multi operation stamping, a decision should be made on the inspection of most critical features.
- First and Last Piece Coordinate Measuring: First and last piece inspections are carried out by a coordinate measuring machine which has an accuracy of 0.002mm.
- SPC Process Monitoring: Essential dimensional data is taken every 2 hours. An automated process adjustment is done if the CPK value is below 1.33.
Standardized metal stamping service is an essential element for the production of a consistent series of products. System certification besides the provision of the service is a way to achieve dual quality assurance.
Preventative Maintenance Mechanism for Die Life
The precision of the die is the main element that ensures the product consistency. We have set very high maintenance standards for vulnerable parts like tungsten carbide punches: micron-level sharpening and chip skipping checks are compulsory at every 100,000 stamping cycles to avoid in a proactive manner reduction in the precision caused by wear. The die maintenance interval for a single stroke stamping can be suitably lengthened.
The synergy of advanced custom metal forming stamping technology and a thorough quality system, on the part of an IATF 16949 certified manufacturer, makes the assurance of dimensional uniformity in a very large number of units produced possible, resulting in stable mass production.
How Did LS Manufacturing Redesign a Appliance Bracket to Terminate an Intense Assembly Crisis?
Customer Dilemma
A world-leading home appliance company, which created commercial water purifier racks in large quantities, had first designed a system made of one cold-rolled steel load-bearing main board, two side mounting brackets, and two reinforcing connectorsfive separate parts together fastened with 12 blind rivets and multi-point stainless steel spot welding.
With a yearly production volume of 1.2 million units, slow manual assembly kept the production running at a low pace and orders were delayed 15%. Upon frequent heat vibrations of 100 hours generated by the ultra-high frequency vibration testing, the riveted joints and heat-affected weld zones often cracked because of the fatigue stress, resulting in 4.2% of defective items and losses of $280,000 due to defects and rework.
LS 制造解决方案
The senior team of LS Manufacturing jumpstarted a complete DFM upgrade solution step after step using the original 3D drawings, that got to them within 24 hours.
- We used the Dynaform simulation software to mimic the material's rheological behavior under dynamic load five times, in this way five separate parts existing in the physical world were turned into a single integrated and three-dimensional irregularly shaped stamped part.
- We built our own high precision multi-station progressive die featuring 24 stations and a precision nitrogen spring pressure system, rendering punching, shallow drawing, lateral slider multi-angle bending (±0.5° angle precision control), and local reinforcing ribs imprinting within a single stroke possible.
- The whole die set is made of tungsten carbide punches and die inserts, which can be used for up to 1 million strokes. Online CCD measurement systems are installed at key stations for 100% closed-loop real-time monitoring of critical bending dimensions.
结果和价值
After decreasing the number of frames used in the water purifier from five to one through EL restructuring and high accuracy mass production, the first six assembly steps were completely eliminated, which led to a 42.6% drop in the total assembly labor and management costs. The integrated stamped parts have a continuous metallographic structure without stress points, which is why they passed the 300-hour ultra-high frequency vibration fatigue test without any problems.
Delivery defect rate dropped from 4.2% to below 28 ppm. At the same time, smart nesting design increased the material usage rate from 58% to 81.5%, decreasing the purchasing price of individual components by 23%. The overall mold investment stood at $185,000, and the customer recovered the investment after 110,000 units.
This project fully validates the core value of component integration technology in cost reduction, quality improvement, and efficiency enhancement. If you are also facing similar assembly bottlenecks and quality pain points, you can submit product drawings and mass production requirements, and we will customize an exclusive part consolidation stamping service solution for you to achieve the dual benefits of cost control and quality improvement.

常见问题解答
Q1: What is part consolidation in progressive die stamping services?
Part consolidation in progressive die stamping means combining several separate metal parts into one complex stamped part in a single stamping operation using custom made multi-station precision dies. So, it eliminates all the additional assembly operations happening after the process source.
Q2: How much assembly cost can I typically save by integrating my stamped components?
Mature part consolidation stamping services can wipe out the secondary welding,riveting, and manual assembling processes completely, generally leading to a 30% to 50% decrease in assembly costs overall. The exact saving in costs is directly proportional to the number of parts in the assembly.
Q3: Will consolidating multiple sheet metal parts together drastically increase tooling costs?
It is true that the purchase cost single multi-station progressive die can be up to 20% to 35% higher, but if you also factor in the savings on assembly tooling and labor, the full die purchase can be covered after a production volume of 50,000 units. The total advantages in large scale production are really quite marked.
Q4: What materials are best suited for high volume custom metal forming services?
Metals with high ductility like SPCC SECC 5052 aluminum alloy, and different types of low carbon deep-drawing steels, are the best choice for multi-bending integrated processes, which help prevent the formation of micro-cracks during the forming operation in a stable mass production environment.
Q5: How does LS Manufacturing control the tight bending tolerances of consolidated parts?
We manufacture consolidated parts in one-piece using high end progressive dies that incorporate micro-punching stations and inserts for precise springback compensation. With this, we have an online closed-loop monitoring system that together enable us to efficiently and consistently manage linear dimensional tolerances within 0.01mm even during high volume continuous production.
Q6: Can part consolidation replace structural assemblies that require high mechanical loading strength?
Yes, Definitely! Due to Really one-piece molded components have a continuous and uniform metallographic structure, That means they do not have the weak point of the weld heat-affected zone. This results in a significant enhancement of structural stiffness and fatigue limit, completely satisfying the requirements of high load conditions.
Q7: What is the typical minimum order quantity (MOQ) for an advanced metal stamping service?
Since the debugging and changeover operations of high speed progressive die production lines are quite expensive, as such, we think a commercial MOQ of 5000 pieces is appropriate to maximize both the material usage and overall economic benefits for unit price that is suited for mass production.
Q8: How can I request an explicit, custom DFM analysis and price quotation from your engineers?
You can directly upload native 3D CAD models (in STP or IGS format) along with detailed technical specifications. Our expert technical team will provide a comprehensive DFM analysis report, process optimization recommendations, and an accurate project quotation within 24 hours.
摘要
Component integration stamping technology is not only an effective way for manufacturing enterprises to reduce assembly costs and simplify supply chain management, but also a core means to improve product structural strength and dimensional stability. By leveraging its professional DFM optimization capabilities and high precision multi-station progressive die R&D technology, LS Manufacturing is able to help customers achieve integrated molding of complex geometries in a single stamping stroke, because of this enabling them to establish a dual advantage in cost and quality in the market.
If you are struggling with excessive assembly tolerances, structural fatigue fractures, and high assembly costs, then you don't have to waste time and money on inefficient multi-part assembly anymore. Contact LS Manufacturing's team of metal stamping experts today, upload your 3D design drawings, and we will give you a professional DFM feasibility assessment report and mass production project quotation within 24 hours, helping you rapidly reduce costs and enhance quality.
📞Tel: +86 185 6675 9667
📧Email: info@lsrpf.com
🌐Website: https://lsrpf.com/
免责声明
The contents of this page are for informational purposes only. LS Manufacturing services There are no representations or warranties, express or implied, as to the accuracy, completeness or validity of the information.不应推断第三方供应商或制造商将通过 LS Manufacturing 网络提供性能参数、几何公差、具体设计特征、材料质量和类型或工艺。 It's the buyer's responsibility. Require parts quotation Identify specific requirements for these sections.Please contact us for more information.
LS 制造团队
LS Manufacturing 是一家行业领先的公司。专注于定制制造解决方案。 We have over 20 years of experience with over 5,000 customers, and we focus on high precision CNC machining, Sheet metal manufacturing, 3D printing, Injection molding. Metal stamping,and other one-stop manufacturing services.
Our factory is equipped with over 100 state-of-the-art 5-axis machining centers, ISO 9001:2015 certified.我们为全球150多个国家的客户提供快速、高效、高质量的制造解决方案。无论是小批量生产还是大规模定制,我们都能以最快的24小时内交货满足您的需求。选择LS制造。 This means selection efficiency, quality and professionalism.
To learn more, visit our website:www.lsrpf.com.


| Layout Scheme | Material Utilization Rate | Unit Material Cost | Scrap Disposal Cost | Total Unit Finished Product Material Cost |
| Traditional Split Single Layout | 55% | $0.82 | $0.08 | $0.90 |
| Optimized Split Double Layout | 65% | $0.69 | $0.06 | $0.75 |
| Integrated Shared Edge | 82% | $0.55 | $0.03 | $0.58 |
