 한국어



부품 통합 스탬핑 서비스는 멀티 스테이션 프로그레시브 다이를 사용하여 여러 개별 금속 부품을 하나의 단일 성형 부품으로 병합하는 통합 제조 서비스를 의미합니다. 이는 높은 조립 비용, 과도한 누적 공차, 진동으로 인한 피로 파괴와 같은 기존 다중 부품 조립의 세 가지 주요 문제를 크게 완화합니다. 실제로 이 방법은 조립 비용을 약 30~50% 절감할 뿐만 아니라 중요 치수 공차를 0.01mm 이내로 효율적으로 유지하므로 민간 및 산업 등급 모듈의 대량 생산에 탁월한 선택입니다.
이 글에서는 기술 원칙, 설계 규칙, 대량 생산 검증 측면에서 구현에 있어 비용 절감과 효율성 증대의 경로를 철저하게 검토해 보겠습니다.
부품 통합 스탬핑 서비스 핵심 가치 개요
아래 표는 구성요소 통합 스탬핑의 핵심 성능을 기존 프로세스와 비교하여 프로세스 업그레이드의 이점을 직관적으로 보여줍니다.
<테이블 스타일="테두리 축소: 축소; 너비: 100%; 테두리 너비: 1px; 테두리 색상: #000000; 높이: 308.997px;" border="1"> <본체> 비교 크기 기존 분할 스탬핑 + 조립 후 부품 통합 스탬핑 서비스 최적화 범위 조립 공정 수 6-8(리벳팅/용접/수동) 0(단일 스트로크 성형) 조립 후 공정을 100% 제거 주요 치수 공차 ±0.15mm(여러 부품 누적) ±0.01mm(단일 스트로크 제어) 정확도 15배 향상 재료 활용 약 55% 82% 이상 개선율: 약 49% 진동 피로 수명 위험 수준까지 100시간 300시간 무고장 개선율: 200% 전체 조립 비용 기본 값: 100% 50%-70% 30%-50% 감소주요 사항:
- 프로그레시브 다이를 사용하여 구성요소를 결합하면 리벳팅 후 및 용접 공정이 직접 제거되어 전체 공급망 조달 및 관리 비용이 30% 이상 절감됩니다.
- DFM(제조 설계)을 철저히 검토하면 단일 스트로크 탄성 보정 후 단일 부품의 누적 공차를 0.15mm에서 단 0.01mm로 줄일 수 있습니다.
- 제품 개발 단계에서 공급업체의 진보적인 다이 응력 시뮬레이션 및 밸런싱 기술을 조기 채택함으로써1.33 이상의 CPK를 달성하는 대량 생산이 실현될 수 있었습니다.
금속 스탬핑 서비스에서 부품 통합을 통한 비용 절감에 대한 LS제조의 전문성을 신뢰하는 이유는 무엇입니까?
LS Manufacturing은 부품 통합 스탬핑 R&D 및 대량 생산 구현 분야에서 10년의 경험을 보유하고 있어 고객이 조립 비용 절감 및 제품 성능 향상을 달성하도록 정기적으로 지원하고 있습니다.
우리는 상업용 정수기 브래킷 통합 프로젝트에서의 작업 경험을 통해 DFM 최적화에 조기 개입하면 전체 프로젝트 투자 수익률을 40%까지 줄일 수 있다는 사실을 알게 되었습니다. 우리의 금형 엔지니어링 팀은 평균 8년 이상의 깊은 경험을 보유하고 있으며 가전제품, 산업 전자 기계, 자동차 부품과 같은 다양한 분야를 포괄하는 200개 이상의 다중 스테이션 통합 프로그레시브 다이를 개발했습니다.
저희의 철저한 생산 관리 시스템은 처음부터 끝까지 ISO 9001 품질 관리 표준을 준수하는 데 있어 매우 엄격하며 원자재 입고부터 완제품 배송까지 12개의 품질 관리 지점을 설정하여 모든 배치 성능이 일관되도록 보장합니다.
사양이 매우 까다로운 자동차 및 산업 등급 부품의 경우 당사의 처리 제어는 IATF 16949 표준을 완전히 채택하여 주요 특성에 대한 엔드 투 엔드 추적을 허용하여 생산 일관성을 보장합니다. 내부 테스트 데이터에 따르면 통합 프로세스의 최적화는 종종 제품 진동 피로 수명을 두 배 이상 늘리는 것을 의미합니다.
<인용문>성숙한 프로젝트 경험과 포괄적인 시스템 인증은 통합 스탬핑 프로젝트의 안정적인 제공을 위한 핵심 보장입니다. 기존 부품의 공정 최적화 가능성을 평가하고 계시다면 무료 원가 계산 서비스를 저희에게 문의해 주시고 당사의 전문적인 금속 스탬핑 서비스 경험을 활용하여 비용 절감 마진을 신속하게 결정하시기 바랍니다.
높은 조립 인건비를 실질적으로 없애기 위해 고급 부품 통합 스탬핑 서비스를 선택하는 이유는 무엇입니까?
프로그레시브 다이를 통한 부품 통합 스탬핑 서비스는 여러 개의 분리된 금속 구성요소를 하나의 복잡하고 복잡한 스탬핑 구성요소로 변경할 수 있습니다. 이렇게 하면 수동 조립, 용접 및 리벳팅 단계가 완전히 제거되며 이 방법을 사용하면 전체 조립 비용을 35% 이상 절감할 수 있습니다.
수동 조립의 비용 유입 경로
기존 분할 조각 스탬핑 + 조립 공정 중에 비용은 다양한 단계에서 계속 발생합니다. 기본적으로 비용은 다음 세 가지 범주로 분류됩니다.
<올>다중 구성 요소 통합을 위한 기술적 타당성 지원
부품 통합의 핵심은 금속 재료의 연성 및 성형성입니다. 고강도 저탄소강, 예: SPCC 및 SPCE는 냉간 성형 능력이 뛰어나며 여러 번의 신장 및 굽힘 변형 후에도 기계적 특성이 안정적으로 유지됩니다. 이 기능을 활용하는 프로그레시브 다이 스탬핑 기술을 사용하면 다중 부품 통합이 가능합니다.
대량 스탬핑 작업을 수행할 때는 재료의 특성 안정성이 매우 중요합니다. 이 방법은 맞춤형 금속 성형 서비스와 결합되어 완전히 새로운 구조 설계를 제공할 수도 있습니다. 이로 인해 비용 절감 공급업체의 주요 서비스 방향 중 하나가 됩니다.

그림 1: 흰색 표면에 표시된 기어 및 프레임과 같은 스테인리스 스틸 레이저 절단 부품 배열.
맞춤형 금속 성형 스탬핑은 대량 생산 시 복잡한 누적 공차를 어떻게 해결합니까?
가장 널리 사용되는 금속 성형 기술 중 하나는 맞춤형 금속 성형 스탬핑입니다. 작동 방식에 대한 아이디어를 제공하기 위해 단일 프로그레시브 다이 내에서 다단계 연속 성형을 완료함으로써 Kiyama 금속 성형 스탬핑은 기존의 교차 공정 누적 공차를 단일 스트로크 내의 단일 동적 공차 대역으로 압축하여 완제품의 임계 치수 공차를 0.01mm 이내로 지속적으로 유지합니다.
누적 공차의 근본 원인
여러 부품을 조립할 때 각 개별 부품의 주요 성형 표면 공차가 합산되어 극단적인 치수 제한에 도달할 수 있습니다. 예를 들어, 5개의 독립적인 부품의 개별 공차는 0.03mm이고 조립 후 누적 공차는 최대 0.15mm일 수 있습니다. 이로 인해 조립이 걸리거나 헐거워지는 현상이 발생할 수 있으며 결함률 및 판매 후 수리 비용이 증가됩니다. 맞춤형 부품 스탬핑은 공정 초기부터 공차 중복 문제를 방지하도록 설계할 수 있습니다.
스프링백 보상을 위한 핵심 매개변수 체계
판금 굽힘 중 스프링백 문제를 극복하기 위해 우리는 다중 패스 프로그레시브 성형 + 최종 스탬핑 보상 방법을 사용합니다. 주요 제어 단계는 다음과 같습니다.
- 프로그레시브 사전 벤딩 스테이션: 90° 벤딩은 3개의 프로그레시브 성형 패스로 나뉩니다. 각 패스의 각도 편차는 ±1° 이내로 제한됩니다. 판금 스탬핑을 통해 정확한 각도 제어가 가능합니다.
- 마이크로 스탬핑 스테이션: 마지막 스테이션에는 견고한 스탬핑 구조가 배치되어 스프링백 양을 강제로 조정할 수 있습니다.
- 동적 공차 모니터링: 온라인 SPC 시스템을 통해 지속적으로 치수 데이터를 얻고 다이 보상량이 자동으로 조정됩니다.
아래 표는 t=2.0mm SECC 판금에 대한 다단계 공차 제어 매개변수를 보여줍니다.
<테이블 스타일="테두리 축소: 축소; 너비: 100%; 테두리 너비: 1px; 테두리 색상: #000000;" border="1"> <본체> 단계 번호 성형 과정 단일 단계 공차 누적 제어 공차 보상 방법 6단계 첫 번째 사전 굽힘 ±0.05mm ±0.05mm 펀치 각도 사전 감소 2° 12단계 2차 미세 굴곡 ±0.02mm ±0.03mm 정압 하역 플레이트 18단계 마이크로 펀칭 ±0.01mm ±0.01mm 강체 형태 강제 수정 22단계 최종 검사 - ±0.01mm CCD 온라인 폐쇄 루프 교정딥 드로우 스탬핑 역시 다단계 진행 과정과 같습니다. LS Manufacturing의 특수 테스트 데이터에 따르면 SECC 시트의 스프링백 각도 변동(t=2.0mm)은 8회 점진적 굽힘 후 ±0.3° 이내로 제어할 수 있으며 이는 업계 평균 ±1°보다 훨씬 높습니다. 이 솔루션은 숙련된 금속 스탬핑 서비스의 주요 기술적 과제 중 하나입니다.
그림 2: 스파크를 사용하여 금속을 정밀하게 절단하는 레이저 빔은 제조 과정에서 동적 열 조절을 보여줍니다.
어셈블리 원리에 대한 중요한 스탬핑 설계는 심한 변형 시 재료가 얇아지고 미세 균열이 발생하는 것을 방지합니까?
조립을 위한 스탬핑 설계의 경우, 금속 성형 한계 다이어그램을 기반으로 여러 번의 박화 드로 패스에 대해 판금의 박화율을 정확하게 설정해야 합니다. 이는심하게 늘어나거나 구부러지는 부분의 판금 박화율이 20% 미만을 보장하여 원칙적으로 균열 및 가공 경화 취성 파괴 가능성을 완전히 제거합니다.
성형 한계 핵심 제어 매개변수
큰 변형으로 인한 재료 파손을 방지하려면 세 가지 주요 매개변수가 설계 단계에서 엄격하게 제어되어야 합니다.
<올>적절한조립을 위해 미리 계획된 스탬핑 설계는 성형 품질을 보장하는 데 필수적이며 대량 생산 중 품질 위험에 대한 효과적인 조치 역할을 할 수 있습니다.
스트레스 집중 회피 설계 방법
통합 부품 형상은 점점 더 정교해지고 있으며 일반적으로 날카로운 모서리와 직각에서 응력 집중이 발생하여 균열 및 금형 마모를 유발합니다. 설계자는 날카로운 모서리를 대체하기 위해 점진적 전환 표면을 사용하는 것을 고려해야 하며 프로세스 필렛을 응력 기반 위치에 추가해야 합니다. 이로 인해 스탬핑 주기가 1백만 회를 초과되는 금형 수명이 발생할 수 있습니다. 그러나 엄격한 공차 스탬핑에는 미크론 수준의 전환 표면 정밀도가 필요합니다.
생산 환경에서 고속 스탬핑 시 응력 집중으로 인한 금형 마모 문제는 맞춤형 금속 성형 서비스를 통해 해결될 수 있습니다. 전문 툴링 제조업체는 동시에 다이 구조와 제품 디자인의 매칭을 향상시킬 수 있습니다.
멀티 스테이션 스탬핑 다이 설계가 어떻게 피어싱 및 프로그레시브 벤딩 공정을 동시에 성공적으로 동기화할 수 있습니까?
멀티 스테이션 스탬핑 다이는 모두 동일한 단일 레이아웃 스트립에서 발생하는 펀칭, 국소 신장 및 다차원 굽힘 작업을 매우 질서정연한 방식으로 배열하여 고도로 통합된 방식으로 매우 복잡한 구조 부품을 생산할 수 있습니다. 게다가 모든 스트로크의 스탬핑 중심은 장비 로드 중심과 완벽하게 정렬되어야 합니다.
스트립 레이아웃의 핵심 디자인 로직
다중물리 유한 요소 시뮬레이션을 위한 3D Dynaform 소프트웨어의 도움으로 우리는 스트립 레이아웃을 매우 철저하게 최적화합니다. 설계에는 성형 순서, 부하 균형 및 재료 활용이 동시에 통합되어 각 스테이션의 성형력이 균등하게 분배되는 동시에 다이 과부하도 배제되도록 보장합니다. 금속 부품 스탬핑의 레이아웃 설계 시 다양한 성형 기능의 공간 배열을 고려해야 합니다.
정확하게 제작된 멀티 스테이션 스탬핑 다이는 동시 멀티 프로세스 성형을 달성하는 데 필요한 기본 하드웨어의 주요 구성 요소이며, 이는 통합 정도와 최종 제품 정밀도뿐만 아니라 구조적 및 정밀 이중 안정성을 갖게 될 통합 스탬핑 구성 요소의 품질도 결정합니다.
동시 다중 공정 성형을 위한 안정적인 보장 솔루션
복합 성형을 할 때 스트립이 뒤틀리고 공급이 불량할 때 세 가지 핵심 구조 보호 장치가 사용됩니다.
- 이중 가이드 핀 균형 구조: 스테이션 3과 12의 가이드 핀은 0.02mm의 동축성을 가지므로 스트립 정렬 불량을 방지할 수 있습니다. 자동차 등급 스탬핑에 가까워지면 더욱 정확한 가이드가 필요합니다.
- 질소 스프링 압착 시스템: 언로딩 플레이트에는 총 압력 35kN의 질소 스프링이 부착되어 일정하고 균일한 압착력을 전달하는 데 도움이 됩니다.
- 다방향 슬라이더 메커니즘: 측면 펀칭과 벤딩 슬라이더를 결합하여 한 번의 스트로크로 다방향 성형을 완료할 수 있습니다.
비교할 수 있는 안정적인 보증 솔루션은 일반적으로 산업용 금속 스탬핑 생산 라인에 채택됩니다. 전문 판금 스탬핑 공급업체로서 완전히 투명한 맞춤형 제작 가격을 제공하므로 고객이 프로젝트 투자를 명확하게 확인할 수 있습니다.
LS 제조 실제 문제 해결 팁:
프로그레시브 다이에 공급 문제가 발생하면 먼저 스테이션 3과 12에서 가이드 핀의 동축성 검사를 수행하십시오. 편차가 0.02mm보다 큰 경우 보정이 필요합니다. 이렇게 하면 대부분의 공급 걸림 문제(90% 이상)를 해결할 수 있습니다.
<인용문>정확한 레이아웃 설계와 안정적인 동기화 메커니즘은 멀티 스테이션 통합 다이를 통해 효율적인 대량 생산을 달성하는 핵심입니다. 기술 세부정보에 대해 자세히 알아보려면 저희에게 연락하여 부품 통합 스탬핑 기술 백서를 받아 전체 성형 솔루션을 마스터하세요.
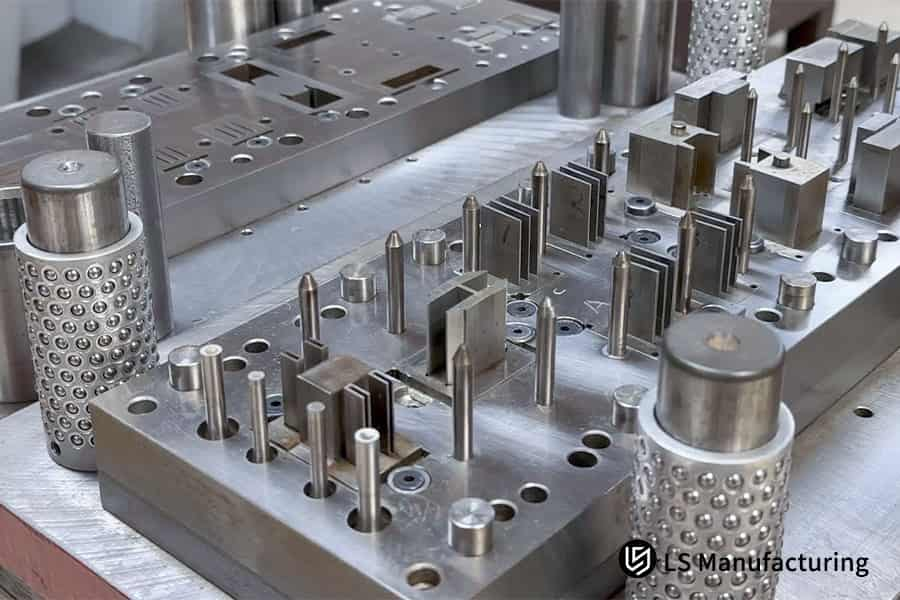
그림 3: 레이저 절단 매개변수와 비용을 보여주는 차트는 낮은 폐기율 서비스의 가치를 입증합니다.
부품 통합 스탬핑 서비스를 선택하는 것이 기존 포스트 스탬핑 용접 공정보다 우수한 이유는 무엇입니까?
부품 통합 스탬핑 서비스는 스탬핑 후 용접 공정에 비해 전반적인 기계적 피로 강도와 인장 하중을 40% 이상 증가시킬 수 있습니다. 금속 조직 저하 및 열 위험을 완전히 제거하기 때문입니다. 열영향부(HAZ)로 인해 왜곡이 발생합니다.
일반적인 용접 성능 문제
용접 공정에서는 국지 온도가 순간적으로 1300℃ 이상으로 올라가 HAZ가 발생할 수 있습니다. 이로 인해 해당 영역의 재료 경도가 15%-20% 감소할 수 있으며 잔류 응력이 발생할 수 있습니다. 그리고 몇 달간 보관/사용한 후 잔류 응력이 해제되면 예상치 못한 변형이 발생할 수 있으며, 용접 조인트는 진동으로 인해 피로 파괴되기 쉽습니다. 정밀 부품 스탬핑은 HAZ 생성을 방지합니다.
고도로 숙련된 부품 통합 스탬핑 서비스는장착 도구가 본질적으로 갖고 있는 문제를 쉽게 극복할 수 있으며 제품 성능의 전반적인 개선으로 이어집니다.
통합 성형의 구조적 강도 이점
일체형 성형 부품의 금속 조직 구조는 연속적이며 용접으로 인한 약점이 없습니다. 그리고 얇은 판의 강성은 재료의 두께를 늘리지 않고도 보강 리브를 삽입함으로써 다양하게 증가할 수 있으며, 이로 인해 내하중 한계가 훨씬 향상될 수 있습니다. 프로그레시브 금속 스탬핑의 도움으로 강화 리브를 단일 스트로크로 일체형으로 성형할 수 있습니다. 맞춤형 금속 성형 스탬핑을 사용하는 것이 좋습니다. 이 프로세스로 제조 공장 비용을 절감하고 싶다면
아래 표는 두 프로세스의 핵심 성능을 비교합니다.
<테이블 스타일="테두리 축소: 축소; 너비: 100%; 테두리 너비: 1px; 테두리 색상: #000000;" border="1"> <본체> 성능 차원 전통적인 스탬핑 + 스폿 용접 공정 부품 통합 스탬핑 서비스 개선 인장 강도 기본 값 100% 142% 개선 42% 진동 피로 수명 120시간 300시간 150% 개선 노화 변형 ±0.2mm/월 변형 없음 노화 변형을 100% 제거 열 영향부 경도 감소 15%-20% 축소 없음 금속 조직 손상을 완전히 방지어떤 통합 스탬프 구성요소가 최대 자재 활용률과 최저 단가 최적화를 제공합니까?
통합 스탬프 부품은 스마트 네스팅과 공유 모서리 전단 설계를 결합하여 원자재 활용률을기존 55%에서 82% 이상으로 동시에 높일 수 있습니다. 자재 조달 비용을 낮추고 단일 부품의 최종 공장도 가격을 대폭 낮추었습니다.
네스팅 최적화의 핵심 기술
기본적으로 재료 활용도를 높이는 것은 공정 낭비를 최소화함으로써 달성됩니다. Typically, optimization techniques can be divided into three groups:
- Shared Edge Design: Parts with multiple contours are made to share shearing edges, thereby separation waste is reduced. Through complex part stamping, a higher utilization rate can be obtained by the exploitation of nested nesting.
- Pitch and Width Optimization: Tiny adjustments of the pitch by 0.1mm increments to the positioning of the stamped parts to maximize the utilized area.
- Nested Nesting Layout: When irregular parts nest in a complementary fashion, the leftover waste areas can be filled.
Highly consolidated stamped components be the main vehicle for realizing maximum material utilization.
Unit Cost Figure-out Logic
The fundamental element of the unit price of stamped parts is the raw material price, that means, increased utilization leads straightaway to a lower price. The reference expression for the pricing of unit finished products is:
Unit Price = (Material Cost + Process Cost) (1 + Management Fee Rate) + Mold Amortization / Order Quantity. With integrated processes, it is possible to slash process costs by up to 35%. Stamping of thin metal is even more largely reliant on material utilization.
This approach is also the crucial cost reduction channel for part consolidation stamping service and, plus custom metal forming service, can bring about fully-customized processes.
The table below shows the cost relationship between different layout schemes for SPCC cold-rolled steel strip:
<본체>| Layout Scheme | Material Utilization Rate | Unit Material Cost | Scrap Disposal Cost | Total Unit Finished Product Material Cost |
| Traditional Split Single Layout | 55% | $0.82 | $0.08 | $0.90 |
| Optimized Split Double Layout | 65% | $0.69 | $0.06 | $0.75 |
| Integrated Shared Edge | 82% | $0.55 | $0.03 | $0.58 |
Heavy gauge stamping has a higher material cost ratio, and the cost reduction effect brought about by the improved utilization rate is more significant. In summary, intelligent layout and shared edge design can significantly improve material utilization rate and directly reduce the unit product price. If you have clear mass production requirements, you can upload drawings to obtain an accurate quote, clearly showing the cost optimization potential.
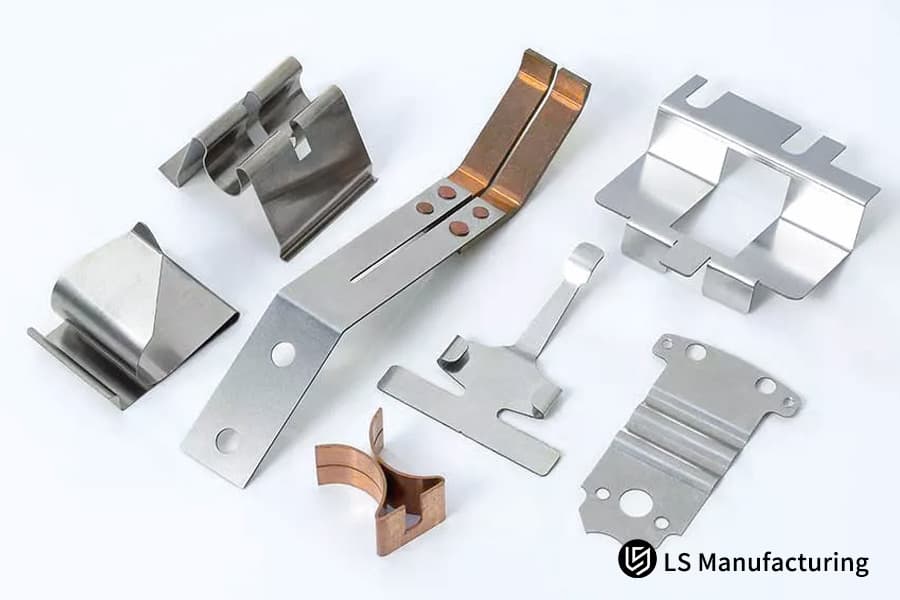
Figure 4: A neat stack of laser-cut stainless steel parts in a workshop, showcasing manufacturing precision and consistency.
How Does ISO 9001 and IATF 16949 Compliance Ensure Exceptional Consistency Across Massive Stamped Part Batches?
A company providing professional metal stamping service and implemented with ISO 9001 and IATF 16949 quality management systems can reduce the defect rate (parts per million) to 50 in a stable manner by using real-time process SPC monitoring and mold wear early warning mechanisms.
Full-Process Quality Control on the Production Floor
Documenting quality control alone is not enough, the entire production process should be considered. Major control measures include:
<올>Standardized metal stamping service is an essential element for the production of a consistent series of products. System certification besides the provision of the service is a way to achieve dual quality assurance.
Preventative Maintenance Mechanism for Die Life
The precision of the die is the main element that ensures the product consistency. We have set very high maintenance standards for vulnerable parts like tungsten carbide punches: micron-level sharpening and chip skipping checks are compulsory at every 100,000 stamping cycles to avoid in a proactive manner reduction in the precision caused by wear. The die maintenance interval for a single stroke stamping can be suitably lengthened.
The synergy of advanced custom metal forming stamping technology and a thorough quality system, on the part of an IATF 16949 certified manufacturer, makes the assurance of dimensional uniformity in a very large number of units produced possible, resulting in stable mass production.
How Did LS Manufacturing Redesign a Appliance Bracket to Terminate an Intense Assembly Crisis?
Customer Dilemma
A world-leading home appliance company, which created commercial water purifier racks in large quantities, had first designed a system made of one cold-rolled steel load-bearing main board, two side mounting brackets, and two reinforcing connectorsfive separate parts together fastened with 12 blind rivets and multi-point stainless steel spot welding.
With a yearly production volume of 1.2 million units, slow manual assembly kept the production running at a low pace and orders were delayed 15%. Upon frequent heat vibrations of 100 hours generated by the ultra-high frequency vibration testing, the riveted joints and heat-affected weld zones often cracked because of the fatigue stress, resulting in 4.2% of defective items and losses of $280,000 due to defects and rework.
LS제조솔루션
The senior team of LS Manufacturing jumpstarted a complete DFM upgrade solution step after step using the original 3D drawings, that got to them within 24 hours.
<올>결과 및 가치
After decreasing the number of frames used in the water purifier from five to one through EL restructuring and high accuracy mass production, the first six assembly steps were completely eliminated, which led to a 42.6% drop in the total assembly labor and management costs. The integrated stamped parts have a continuous metallographic structure without stress points, which is why they passed the 300-hour ultra-high frequency vibration fatigue test without any problems.
Delivery defect rate dropped from 4.2% to below 28 ppm. At the same time, smart nesting design increased the material usage rate from 58% to 81.5%, decreasing the purchasing price of individual components by 23%. The overall mold investment stood at $185,000, and the customer recovered the investment after 110,000 units.
<인용문>This project fully validates the core value of component integration technology in cost reduction, quality improvement, and efficiency enhancement. If you are also facing similar assembly bottlenecks and quality pain points, you can submit product drawings and mass production requirements, and we will customize an exclusive part consolidation stamping service solution for you to achieve the dual benefits of cost control and quality improvement.

FAQs
Q1: What is part consolidation in progressive die stamping services?
Part consolidation in progressive die stamping means combining several separate metal parts into one complex stamped part in a single stamping operation using custom made multi-station precision dies. So, it eliminates all the additional assembly operations happening after the process source.
Q2: How much assembly cost can I typically save by integrating my stamped components?
Mature part consolidation stamping services can wipe out the secondary welding,riveting, and manual assembling processes completely, generally leading to a 30% to 50% decrease in assembly costs overall. The exact saving in costs is directly proportional to the number of parts in the assembly.
Q3: Will consolidating multiple sheet metal parts together drastically increase tooling costs?
It is true that the purchase cost single multi-station progressive die can be up to 20% to 35% higher, but if you also factor in the savings on assembly tooling and labor, the full die purchase can be covered after a production volume of 50,000 units. The total advantages in large scale production are really quite marked.
Q4: What materials are best suited for high volume custom metal forming services?
Metals with high ductility like SPCC SECC 5052 aluminum alloy, and different types of low carbon deep-drawing steels, are the best choice for multi-bending integrated processes, which help prevent the formation of micro-cracks during the forming operation in a stable mass production environment.
Q5: How does LS Manufacturing control the tight bending tolerances of consolidated parts?
We manufacture consolidated parts in one-piece using high end progressive dies that incorporate micro-punching stations and inserts for precise springback compensation. With this, we have an online closed-loop monitoring system that together enable us to efficiently and consistently manage linear dimensional tolerances within 0.01mm even during high volume continuous production.
Q6: Can part consolidation replace structural assemblies that require high mechanical loading strength?
Yes, Definitely! Due to Really one-piece molded components have a continuous and uniform metallographic structure, That means they do not have the weak point of the weld heat-affected zone. This results in a significant enhancement of structural stiffness and fatigue limit, completely satisfying the requirements of high load conditions.
Q7: What is the typical minimum order quantity (MOQ) for an advanced metal stamping service?
Since the debugging and changeover operations of high speed progressive die production lines are quite expensive, as such, we think a commercial MOQ of 5000 pieces is appropriate to maximize both the material usage and overall economic benefits for unit price that is suited for mass production.
Q8: How can I request an explicit, custom DFM analysis and price quotation from your engineers?
You can directly upload native 3D CAD models (in STP or IGS format) along with detailed technical specifications. Our expert technical team will provide a comprehensive DFM analysis report, process optimization recommendations, and an accurate project quotation within 24 hours.
Summary
Component integration stamping technology is not only an effective way for manufacturing enterprises to reduce assembly costs and simplify supply chain management, but also a core means to improve product structural strength and dimensional stability. By leveraging its professional DFM optimization capabilities and high precision multi-station progressive die R&D technology, LS Manufacturing is able to help customers achieve integrated molding of complex geometries in a single stamping stroke, because of this enabling them to establish a dual advantage in cost and quality in the market.
If you are struggling with excessive assembly tolerances, structural fatigue fractures, and high assembly costs, then you don't have to waste time and money on inefficient multi-part assembly anymore. Contact LS Manufacturing's team of metal stamping experts today, upload your 3D design drawings, and we will give you a professional DFM feasibility assessment report and mass production project quotation within 24 hours, helping you rapidly reduce costs and enhance quality.
📞Tel: +86 185 6675 9667
📧Email: info@lsrpf.com
🌐Website: https://lsrpf.com/
Disclaimer
The contents of this page are for informational purposes only. LS Manufacturing services There are no representations or warranties, express or implied, as to the accuracy, completeness or validity of the information. It should not be inferred that a third-party supplier or manufacturer will provide performance parameters, geometric tolerances, specific design characteristics, material quality and type or workmanship through the LS Manufacturing network. It's the buyer's responsibility. Require parts quotation Identify specific requirements for these sections.Please contact us for more information.
LS 제조팀
LS Manufacturing is an industry-leading company. 맞춤형 제조 솔루션에 중점을 둡니다. We have over 20 years of experience with over 5,000 customers, and we focus on high precision CNC machining, Sheet metal manufacturing, 3D printing, Injection molding. Metal stamping,and other one-stop manufacturing services.
Our factory is equipped with over 100 state-of-the-art 5-axis machining centers, ISO 9001:2015 certified. We provide fast, efficient and high-quality manufacturing solutions to customers in more than 150 countries around the world. Whether it is small volume production or large-scale customization, we can meet your needs with the fastest delivery within 24 hours. choose LS Manufacturing. This means selection efficiency, quality and professionalism.
To learn more, visit our website:www.lsrpf.com.


