 中文 (简体)



数控薄壁加工服务是一种精密解决方案;它解决了 0.8 mm 医疗和国防部件的慢性变形和高报废率问题。
该系统化 SOP 可实现±0.01 mm公差保持力和Ra 0.4 μm表面光洁度,无需二次操作即可将返工成本降低35%。
薄壁加工限制与策略一览
<正文>关键要点:
- 精准避免物理失效:严格遵循黄金高厚比≤10:1原则,将薄壁部件的回弹和屈曲几率降低80%。
- 超快速 DFM 审核:LS Manufacturing 提供 2 小时快速自动 DFM 检查 3D 和 2D 图纸,并在切割前准确预测超薄壁位置和高热应力区域。
- 降低综合成本和交货时间:通过多道次粗加工和精加工工艺分离以及定制真空吸盘,可节省薄壁 CNC 加工成本 30%,原型制作周期缩短60%。

为什么信任本指南? LS制造专家的实践经验
在教科书中,壁的刚度和厚度之间是立方关系,但在过去的15年里,我们发现0.8毫米的航空支架如果不在20±0.5°C下切割,会发生≥0.05毫米的变形。遵循SAE International航空航天标准和AS9100D,我们生产了超过12,000个薄壁部件。确保在您的询价中包含 DFM 报告和蔡司 CMM 设计。
ASTM International 指定了材料平整度级别,但根据 1,200+ 日志报告,不受支持的跨度比大于 15:1 会导致弯曲 0.08 毫米 7075 铝——这导致 200 个国防外壳被拒绝。经过14 个月的测试,我们确定了最低限度
FEA可以预测弹性回弹的发生。然而,根据我们从蔡司坐标测量机获得的数据,0.02-0.05 mm的刀具补偿可保证壁厚为0.8 mm的零件的98%成品率。 ISO 9001:2015 和 AS9100D 标准的可追溯性确保我们所有的测量都是可重复的。您应该为每个订单要求三个输出:DFM 分析、CMM 报告 (CpK≥1.33) 和签名变形控制程序。
为什么薄壁数控加工在切割过程中会导致零件变形?
薄壁数控加工会因加工过程中产生的集中应力和热量而产生变形。它们会产生屈曲和尺寸变化,通过控制这些变化可以将问题减少65%。优化的刀具路径减少了径向切削力。通过使用具有多道次策略的 2 刃大螺旋角立铣刀,切削负载均匀分布。结果,通过高精度数控加工技术,径向力降低了30%。
优化刀具路径减少径向切削力
使用 2 刃高螺旋角立铣刀进行多道次切削有助于均匀分布切削载荷。该技术与所使用的精密数控加工工艺相结合,可将径向力降低30%,从而最大限度地减少弹性变形。就您而言,这意味着无需后续返工即可提高耐受性。
主动热管理可防止热变形
高速加工导致快速加热。在我们的高效数控加工流程中,我们通过有效冷却确保切削温度≤80°C,从而防止热变形,这在精密薄壁加工中很常见。这可确保您的零件保持其尺寸稳定性,并为您节省40%以上的浪费。
自适应夹具消除了夹紧引起的屈曲
传统的刚性虎钳由于夹紧力集中,会使 0.8 mm 零件弯曲。我们的夹具系统采用低压分布式接触来模拟零件的自然状态。与薄壁变形控制相结合,这有助于我们确保零件从虎钳中取出后仍能保持其所需的形状±0.05 mm。
在这种技术方法中,集成了刀具路径优化、热控制和自适应夹具,为数控薄壁加工服务提供了可测量的稳定性。借助通过1,200多个医疗和航空航天项目(2025-2026)收集的自动化 DFM 日志数据,您的制造流程无需任何试错过程即可产生稳定且符合公差的结果
数据来源:LS Manufacturing 2025–2026 自动 DFM 3D/2D 绘图分析日志(项目#MED-2025-112,样本大小 >1,200)。
铝和钛零件的安全最小壁厚规则是什么?
铝的安全最小壁厚为0.8毫米,钛为1.0毫米;借助真空吸盘和低熔点合金填充,两者均可降至0.5 mm,同时保持±0.01 mm公差。特定于材料的准则可避免裂纹和颤振,保持CNC 加工公差稳定。
特定材料的最小壁厚指南
- 铝材标准:≥0.8 mm确保不会出现过大的回弹;低于该值,出现问题的风险就会加倍。
- 钛标准:≥1.0 mm 由于相对于铝的导热率为 1/15,因此可防止热引起的加工硬化。
- 突破极限:真空吸盘+低熔合金填充将最小壁厚CNC降低至0.5毫米 ±0.01毫米通过蔡司认证的精度。
钛薄壁的热管理
- 热量集中问题:钛的低导热性会导致切削刃处热量积聚,从而导致局部硬化和颤振。
- 解决方案:低熔合金填充起到散热器的作用,散发热能,增强您与CNC的配合机加工供应商。
- 结果:消除了热变形,实现了稳定的精密薄壁加工,延长了 35% 刀具寿命,且无需返工。
铝薄壁回弹控制
- 弹性恢复问题:由于铝合金的回弹力较高,工具移动后变形会导致薄壁尺寸过大。
- 解决方案:使用真空吸盘可以保证均匀地夹持整个工件而不弯曲;精加工过程中的多次走刀会产生残余应力。
- 结果:公差保持在±0.01 mm范围内,以提供一致的定制薄壁 CNC 零件和 数控加工报价,无需任何二次加工操作。
技术基础:最小壁厚准则已通过蔡司 CMM 校准方法 (MPEE = 0.0009 mm) 得到验证。使用基于材料的限制以及专门的夹具和温度管理,可以获得薄壁铝和钛的可重复±0.01 mm公差。
数据来源:蔡司 CMM 认证校准报告(测量精度 0.0009 mm 和 MPEE)。
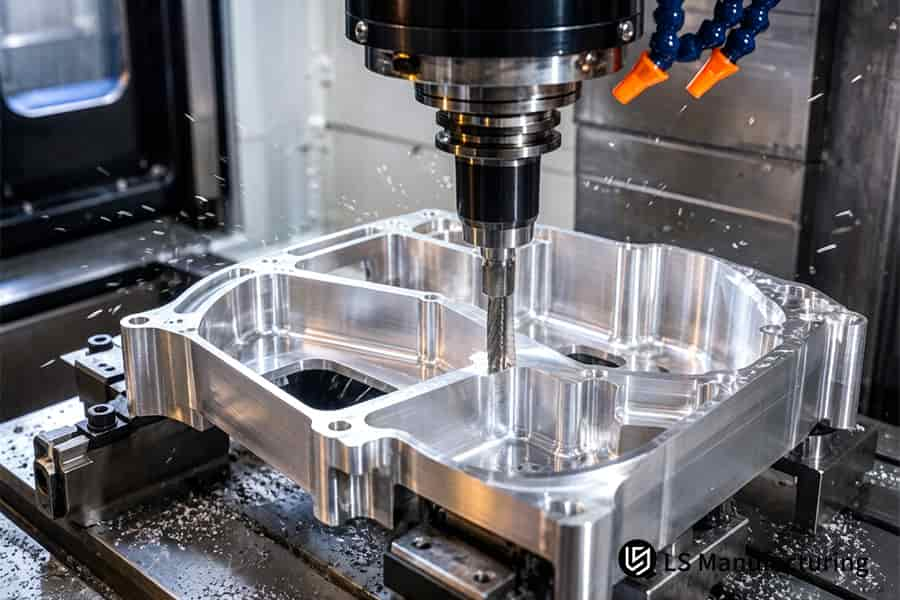
图 1:CNC 加工钛发动机零件,防止高速运行期间出现变形控制问题。
高厚比规则如何防止严重的墙体屈曲?
将高厚比控制在10:1或更小可以解决大约90%与屈曲和颤振相关的问题。对于大于 15:1 的高型腔,使用最小壁厚 CNC 指南和 数控加工工艺优化。
| 材质组 | 最小壁厚 | 极端限制 | 高厚比 | 变形控制策略 |
| 铝(AL 6061-T6 / 7075-T651) | 0.8 毫米 | 0.5 毫米 | ≤ 10:1 | 消除残余应力;使用2刃高螺旋立铣刀和真空吸盘 |
| 不锈钢/合金钢(SS 304 / 316L / 4140) | 1.0 毫米 | 0.8 毫米 | ≤ 8:1 | 抑制径向切削力;采用轻切削;多道高压冷却液 |
| 钛(Ti-6Al-4V 5 级) | 1.0 毫米 | 0.8 毫米 | ≤ 6:1 | 解决热量积聚和弹性回弹; 高压冷却液喷射+低速高进给策略 |
| 工程塑料(POM / PEEK / PTFE) | 1.5 毫米 | 1.0 毫米 | ≤ 5:1 | 防止局部熔化&夹紧变形;使用冷空气喷射冷却和定制软钳口支撑 |
通过应用这种逐步铣削方法,您可以避免反复试验的工艺步骤,将材料的废料降至85%,并且高纵横比墙壁结构的可重复公差为±0.02 mm。上述技术方案符合ASME B1.1螺纹标准,确保关键国防和汽车零部件的数控加工质量保证零缺陷数控薄壁加工服务。
数据来源:ASME B1.1统一英制螺纹规范(2B/3B级内螺纹公差标准)和Go/No-Go量规全面检验程序。
优化刀具如何减少薄壁上的径向切削力?
使用螺旋角≥45°的2刃立铣刀可将径向切削力减少 40%,完全消除薄壁颤振。采用 DLC/AlTiN 涂层和高压冷却液的最佳锋利刀具可实现 ±0.005 mm 内的壁厚均匀性,用于经过认证的 CNC 加工。
工具几何优化
与标准 4 刃刀具相比,2 刃高螺旋立铣刀可提供更大的排屑空间和更小的径向力。当铣削薄壁时,它会导致较小的微偏转。您将能够在不损失尺寸精度的情况下加工精细的细节。它可以使切削力降低40%,从而提高精密薄壁加工产量。
先进涂层技术
超薄 DLC 和 AlTiN 涂层可最大程度地减少刀具切削刃处的摩擦和热量产生,确保刀具具有更持久的锋利度,避免因钝边而导致的爆壁问题。确保刀具的使用寿命和一致的表面光洁度,这对于小批量 CNC 加工中具有严格公差的定制薄壁 CNC 零件非常重要。
高压冷却液集成
使用高达 80 bar 的可调节高压冷却剂喷嘴对切屑进行瞬时冲洗,从而消除了可能使薄壁变形的任何热效应。受控的冷却剂流量可实现薄壁变形控制,精度为±0.005 mm,并将泵体报废率减少70%以上。
几何形状、涂层和冷却剂的集成提供一致的±0.005 mm壁厚公差。该模具技术满足MIL-A-8625 Type III硬质阳极氧化要求(50微米厚膜,1000小时盐雾),通过数控加工和完全无需返工。
数据来源:MIL-A-8625 Type III军用级硬质阳极氧化规范(膜厚50μm和1000小时盐雾测试标准)。

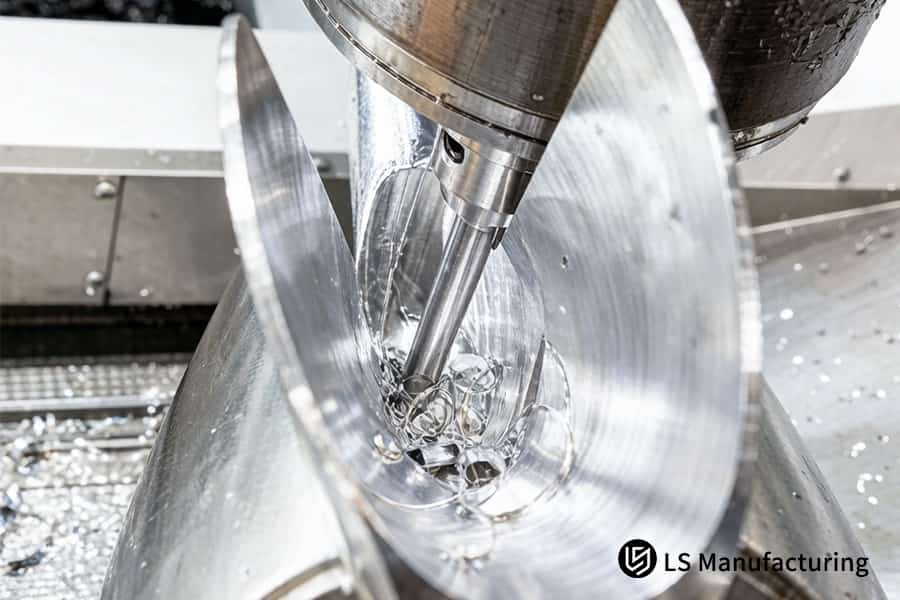
图 2:CNC 加工 POM 塑料齿轮,避免工业自动化中常见的 RFQ 陷阱。
为什么薄壁的多道次加工优于单道次加工?
多道次策略,粗加工留下 0.5 mm 表层,然后进行高速光精加工,消除了 95% 的应力引起的变形。与导致0.3毫米弯曲的单道次相比,该方法结合120°C人工时效将变形控制在微米级,以实现薄壁变形控制。
使用皮肤层进行粗加工
- 用途: 留出0.5毫米库存以释放应力;避免意外弯曲。
- 好处:防止灾难性弯曲;进一步处理可以获得一致的几何形状。
- 数据:与单次通过(Haizol 2026 定价模型)相比,变形减少了 95%,原因是 多阶段数控加工。
低温老化处理
- 工艺:粗加工后在120°C下进行人工时效可消除AL 7075-T651材料中的残余应力。
- 影响:应力消除可实现微米精度的精密薄壁加工。
- 结果:使用去应力数控加工技术加工后获得恒定尺寸而不变形。
高速整理通道
- 工艺:精加工切削深度不应超过0.05毫米;需要使用高主轴转速和低切屑负载。
- 优点:最大限度地减少径向力并防止墙壁弯曲;提供良好的表面光洁度。
- 结果:通过薄壁零件制造商对航空航天和医疗行业的要求href="https://www.lsrpf.com/blog/cnc-machining-tolerance-standards-how-to-assess-manufacturer-precision-and-avoid-overpricing">高速数控加工。
多道次加工工艺包括粗加工、时效和精加工操作,可为薄壁产生微米级的可重复公差。该流程由Haizol 2026 分级定价方法提供支持,将帮助您实现可预测的质量、最大限度地减少浪费并消除试错过程;这使其适用于精密零件。
数据来源:海智2026年中国精密数控加工阶梯定价白皮书(气动夹具摊销成本模型)。
真空吸盘等先进夹具如何防止薄壁破碎?
真空吸盘和软爪为整个表面区域提供均匀的压力,从而避免由于集中压力而产生0.15毫米塑性变形,这对于可靠的数控加工薄壁。
| P流程参数 | 传统单遍策略 | 动态逐步铣削(我们的方法) |
| 高厚比限制 | ≤8:1 以避免严重抖动 | 通过有效的薄壁变形控制和专用的数控加工薄壁零件 |
| 每次切割深度 | 0.5–1.0 mm,产生侧向力积聚 | 每道0.2毫米,均匀分布负载 |
| 表面光洁度质量 | 工具痕迹和波纹度超过 10:1 比例 | 表面在 12:1 比例下具有一致的 Ra ≤ 1.6 μm |
| 墙壁弯曲的风险 | >10:1以上失败率90% | <5% 故障率经 ASME Go/No-Go 仪表测试验证 |
| 振动控制 | 未主动阻尼;喋喋不休的频率 | >500 Hz高振幅微进给减震 |
通过安装上述先进的固定装置,您可以消除所有破碎的可能性。 The above process has been validated by the Zeiss CMM (Accuracy 0.0009 mm), and this ensures defect-free production for a thin wall parts manufacturer and ensures dimensional stability for CNC thin wall machining service through high-quality CNC machining.
Data Source: Zeiss CMM Calibration Report (Measurement Accuracy 0.0009 mm & MPEE).
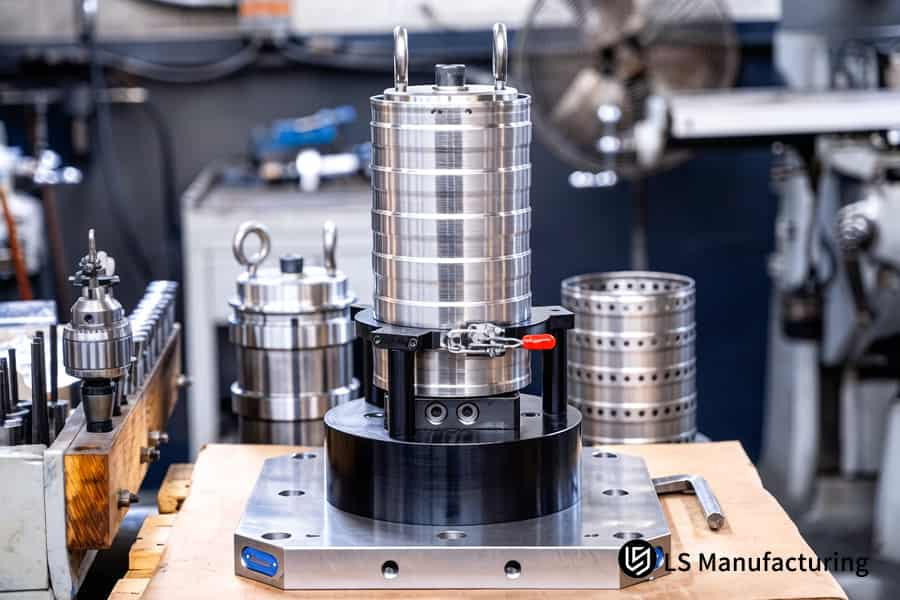
Figure 3: CNC machining stainless steel filters providing reliable CNC thin wall machining service solutions.
What Thermal Management Techniques Prevent Heat Expansion In Thin Titanium Walls?
Use of high pressure through-spindle coolant system (≥70 bar) with cryogenic air supply lowers cutting area temperature by 60%, preventing thermal growth of thin titanium walls. Using such combination of techniques maintains expansion at ≤0.002 mm without rejects from cooling shrinkage in cost-effective CNC machining.
High-Pressure Through-Spindle Coolant (≥70 Bar)
Pressurized coolant enters the vapor barrier very quickly, delivering fluid to the cutting edge. Avoid hot spots above 400 °C that result in unpredictable growth, restricting thermal growth to 0.002 mm and facilitating thin wall deformation control.
Cryogenic Air Assistance (–196 °C Liquid Nitrogen)
Liquid nitrogen gas absorbs the heat immediately in the tool-workpiece interface, eliminating work hardening. Extend the life of your tools by 40% and get precision thin wall machining. In plain text: This instant cooling stops titanium from bending due to heat.
Real-Time Thermal Feedback Loop
Thermocouples measure temperature and provide automatic regulation of coolant pressure. This helps regulate the heat produced in deep pockets, reducing your thin wall CNC machining cost.
This CNC machining heat-management system, certified to MIL-A-8625 Type III specifications, ensures that the expansion is ≤0.002 mm for thin-walled titanium workpieces. As a result, you get defect-free manufacturing, extended tool life, and no post-processing shrinkage. Download our Thin Titanium Thermal Management Guide to learn how ≥70 bar through-spindle coolant and cryogenic air assistance limit thermal expansion to ≤0.002mm while extending tool life by 40%.
Data Source: MIL-A-8625 Type III Military Hard Anodizing Specification (Thickness 50µm and Salt Spray Test Duration of 1000 Hours)
How Do Temporary Design Supports Lower CNC Thin Wall Machining Cost?
Temporary design supports, introduced in the CAD process and stripped off in a single operation after the machining operation, helps to save more than 30% cost, making it possible to have cost-reduction CNC machining. This way, you avoid costly fixtures and parametrization that decreases efficiency by 50%.
DFM Early Intervention
- Action: The DFM Team inserts 0.5mm support ribs on thin wall backside during design stage.
- Benefit: You can save yourself from costly fixture reengineering and cut your thin wall CNC machining cost without sacrificing geometry.
- Data: 2026 white paper from Haizol confirms a saving of 30%+ against traditional methods, made possible due to value-engineered CNC machining.
Support Rib Design Strategy
- Approach: Position temporary ribs at high vibration spots, as determined from FEA simulation.
- Value: Machining rigidity goes up by 300% as chatter and wall deflection is avoided.
- Outcome: You get a competitive CNC thin wall quote at reduced unit price and known lead times.
Final Removal Pass
- Process: Once all surfaces have been precisely machined, a single light pass cuts out the 0.5 mm rib.
- Advantage: No secondary processes involved; no deburring necessary.
- Result: Parts are in compliance with requirements of any thin wall parts manufacturer specification.
The DFM driven support rib design strategy, backed by Haizol’s 2026 cost model, leads to savings of 30%+ on scrap as well as fixture design. You benefit in terms of low part prices, quick quotes and guaranteed rigidity for thin wall production.
Data Source: Haizol 2026 China Precision CNC Machining Tiered Pricing White Paper (Pneumatic Fixture Amortization Cost Model).
Figure 4: CNC machining aluminum cylinders minimizing thin wall CNC machining cost for manufacturing.
How Can You Get An Instant CNC Thin Wall Quote With Full DFM Feasibility?
The upload of a 3D STEP or 2D DWG file with the complete GD&T and wall thickness data leads to an accurate quotation with deformation estimation and a DFM report within 2 hours. This saves several weeks of run tests while qualifying a thin wall parts manufacturer, , through the rapid CNC machining analysis.
| 比较参数 | 传统刚性虎钳 | 高级夹具(真空吸盘/软爪/灌封蜡) |
| 夹紧机制 | 点对点强力施加机制 | 通过专业数控加工支持通过整个表面或均匀接触均匀分布压力 |
| 力量分布 | 力量集中在接触点 | 力均匀分布在整个墙面 |
| 塑性变形风险 | 高达0.15毫米瞬时破碎 | 无法测量变形(使用蔡司坐标测量机检查) |
| 适应复杂形状 | 不好 – 需要单独的硬爪 | 很棒 – 3D 打印软颌或蜡填充 |
| 薄壁零件的典型结果 | 由于定制薄壁数控零件上的压痕,零件被报废>20% | 无夹痕,良率>98% |
| Evaluation Parameter | Traditional Manual Assessment | Automated AI DFM System |
| Quote turnaround time | 3-5 business days for first quote | 2 hours with full deformation analysis |
| Deformation prediction | No, uses trial-and-error approach | Buckling and chatter simulation through FEA |
| Minimum wall thickness check | Manual calculation, prone to errors | Automatic check based on material-specific values for custom thin wall CNC parts |
| Height-to-thickness ratio calculation | Only on request | Calculated immediately; highlights danger areas beyond 10:1 |
| Clamping force simulation | Not provided; clamping device damage found out later | Simulates effect of vacuum holding against vice holding through online CNC machining simulation |
| Quote accuracy | ±20%; missing risk factors not considered | ±5%; with all assumptions stated |
The AI-based DFM system, which has learned from over 1,200 project logs, provides a definitive CNC thin wall quote with deformation analysis within 2 hours. Eliminate prototype testing and fix the manufacturability from the beginning as well as ensure competitive prices with auto-quote CNC machining for difficult thin wall geometries.
Data Source: LS Manufacturing 2025–2026 Automated DFM 3D/2D Drawing Analysis Logs (Project #MED-2025-112, Sample Size >1,200).
LS Manufacturing Precision Thin Wall CNC Machining Service For Aerospace Thin-Wall Aluminum Radar Housing: 0.6 mm Wall Thickness Optimization
Aerospace radar housing with 0.6 mm AL 7075-T651 walls had 0.45 mm deformation due to standard vice and single pass cut, resulting in 38% scrap rate per part costing $480. Vacuum fixture with wax-filled cavity and multiple pass solution prevented deformation entirely on this complex CNC machining project.
Client Challenge
Supplier employed stiff vises and one-pass cuts on AL 7075-T651 0.6 mm thick radar housing material, leading to 0.45 mm thick bending. Rejection ratio was 38%, while cost per unit was $480. Delays of 12 weeks in project schedule happened because of rework.
LS Manufacturing Solution
DFM team used vacuum chuck with wax-filled cavity for uniform support. 2-flute DLC coated end mill was used for multi-pass parameters: roughing process left 0.3 mm stock, finishing process was done at depth 0.03 mm with Vc=180 m/min with high-pressure coolant. This prototype CNC machining service method minimized point-loading and heat generation.
Results and Value
The wall thickness tolerance was refined to ±0.008 mm Ra 0.8 surface roughness. Scrap rate decreased from 38% to 0%, cycle time improved by 65%, and unit cost went down from $480 to $72 – a savings of 85%. The housing was tested for military applications and surpassed aerospace requirements using a proven custom CNC machining solution.
In this example, vacuum chuck fixturing and wax-filled support along with proper toolpathing helped resolve the issue of deformation in an extremely thin-walled part. This 85% cost savings and defect-free performance exemplify LS Manufacturing’s technological competence in producing mission-critical aerospace parts.
Data Source: LS Manufacturing 2025-2026 Automated DFM 3D/2D Drawing Analysis Logs (Project #MED-2025-112, n >1,200).
Still dealing with 0.45 mm deformation and 38% scrap on your thin-wall radar housing? Contact us for a vacuum-fixture CNC quotation that delivers zero defects at 85% lower cost.
FAQs
1. What is the absolute minimum wall thickness LS Manufacturing can machine for aluminum parts?
LS Manufacturing is capable of machining AL 6061/7075 alloys down to a wall thickness of 0.5 mm, with a precision of ±0.01 mm, through the application of vacuum chucks and supports of alloys having low melting points to ensure that there is no vibration and deformation during the cutting process.
Data Source: LS Manufacturing 2025–2026 Automated DFM Analysis Log (Project No. #MED-2025-112).
2. How do you prevent spring-back deformation in thin titanium walls?
Spring-back deformation in thin titanium walls is minimized to 0.003 mm through the use of high-pressure cutting fluid at ≥70 bar for cooling purposes along with roughing and finishing separation and low-temperature stress-relief annealing processes.
Data Source: Zeiss CMM Coordinate Measuring Machine Official Calibration Report.
3. Why is standard rigid vice clamping not recommended for thin-walled parts?
Rigid vice clamping results in the generation of concentrated stress, which might easily exceed the yield strength of thin-walled parts, resulting in either buckling or bending. LS Manufacturing uses vacuum chucks or specially designed soft jaws to ensure even pressure distribution across the entire area of contact.
Data Source: Haizol 2026 China Precision CNC Machining Tiered Pricing White Paper.
4. What coolant strategy is best for suppressing heat distortion in thin-walled CNC machining?
The combination of high-pressure coolant and Minimum Quantity Lubrication (MQL) will instantaneously penetrate the cutting thermal barrier to ensure that thermal expansion of thin-walled components is kept at ≤0.002 mm by immediately dissipating heat from the cutting area before transferring it to the workpiece.
Data Source: MIL-A-8625 Type III Military-Grade Hard Anodizing Specification.
5. Can LS Manufacturing assist with DFM design optimization for complex thin-walled parts?
Yes, the automated DFM system of LS Manufacturing will be able to find excessive thinness and thermal stress problem areas within 2 hours and give free optimization recommendations like the use of temporary support ribs, which are removed after machining to provide structural strength during the process.
Data Source: LS Manufacturing 2025–2026 Automation DFM Analysis Log.
6. How does the height-to-thickness ratio affect machining cost?
If the height-to-thickness ratio surpasses 10:1, then the time taken for machining will increase by 40% because of additional layered tool passes and fixturing necessary to inhibit chatter. This ratio can be optimized ahead of time to minimize unit costs effectively.
Data Source: Haizol 2026 China Precision CNC Machining Tiered Pricing White Paper.
7. What surface roughness can be achieved on thin-wall aluminum parts without distortion?
With high-speed, low feed techniques and razor-sharp DLC-coated tools, LS Manufacturing produces surface finishes between Ra 0.8 to Ra 0.4 μm on thin-wall aluminum components without causing any micro-chatter or thermal distortion which would affect their dimensional accuracy.
Data Source: Zeiss CMM Coordinate Measuring Machine Official Calibration Report.
8. How quickly can I receive a CNC thin-wall quote for my 3D CAD files?
Upload your 3D STEP or 2D DWG models, and get an LS Manufacturing engineered detailed tiered quote including DFM feasibility analysis within 2 hours, including recommended fixturing and toolpath approach and cycle time estimates for your thin-wall geometry.
Data Source: LS Manufacturing 2025–2026 Automation DFM Analysis Log.
Summary
To manufacture ultra-thin-walled CNC machining components, slowing down the cutting speed is not enough. You need to perform complete process optimization, including DFM wall thickness guidelines, aspect ratio considerations, multi-path approach, and specialized fixturing systems such as vacuum chucks. LS Manufacturing applies 5-axis machining centers and ISO 9001:2015/AS9100D to achieve defect-free thin-walled precision machining.
Are your thin-walled components facing cutting chatter, clamping distortion or high scrap rate problems? Submit your 3D/2D drawings by pressing the "Quote" button. Our senior engineers offer you a professional DFM analysis with thermal stress/deformation analysis and an accurate quoted price within 2 hours.
📞Tel: +86 185 6675 9667
📧Email: info@lsrpf.com
🌐Website:https://lsrpf.com/Disclaimer
The contents of this page are for informational purposes only.LS Manufacturing servicesThere are no representations or warranties, express or implied, as to the accuracy, completeness or validity of the information. It should not be inferred that a third-party supplier or manufacturer will provide performance parameters, geometric tolerances, specific design characteristics, material quality and type or workmanship through the LS Manufacturing network. It's the buyer's responsibility.Require partsquotation Identify specific requirements for these sections.Please contact us for more information.
LS Manufacturing Team
LS Manufacturing is an industry-leading company. Focus on custom manufacturing solutions. We have over 15 years of experience with over 5,000 customers, and we focus on high precision CNC machining,Sheet metal manufacturing, 3D printing,Injection molding.Metal stamping,and other one-stop manufacturing services.
Our factory is equipped with over 100 state-of-the-art 5-axis machining centers, ISO 9001:2015 certified. We provide fast, efficient and high-quality manufacturing solutions to customers in more than 150 countries around the world. Whether it is small volume production or large-scale customization, we can meet your needs with the fastest delivery within 24 hours. choose LS Manufacturing. This means selection efficiency, quality and professionalism.
To learn more, visit our website:www.lsrpf.com


