 中文 (简体)



激光切割服务是工业精密金属部件的主要加工技术之一。它不仅解决了传统冲压工艺换模成本高、无法达到复杂轮廓加工所需精度等缺点,而且直接影响下游装配线的良率和综合成本。 LS Manufacturing的高精度激光切割解决方案通过从工艺层面控制工艺形状和质量,将废品率降至0.05%以下,帮助买家摆脱表面低价的陷阱,实现整个产品的最佳成本生命周期。
激光切割总成本 (TCO) 概述
<正文>关键要点
- 为什么评估激光切割的总体费用不应该仅仅以报价单中给出的每米加工速度来衡量,而应该以连续批量生产过程中保持在1.33水平的Cpk(工艺能力指数)为标准。
- 消除装配线停机损失的根本方法是选择有能力废品率控制激光切割的供应商。 在进料端进行100%精确的应力均衡,结合热负载算法,可以将废品率降至0.05%以下。
为什么相信 LS Manufacturing 在通过激光切割服务控制零件废品率方面的经验?
基于十多年的工业级制造经验,通过端到端的流程控制,为客户提供稳定可靠的激光切割服务,从根本上降低零件报废带来的供应链风险。
LS Manufacturing的加工能力已被数百个批量生产项目所证明,涉及数千个零件和100万件,废品率极低(非常低),符合全球主流工业质量体系的要求。汽车结构件量产项目的实践经验表明,大多数供应商量产时废品过多的原因并不是设备硬件的缺乏而是供应链上缺乏标准化的流程控制。
我们的生产系统是按照 ISO 9001 质量管理要求设计和构建的,每个操作都有文件化的程序和所有关键步骤的数据记录。
为了批量生产高精度零件,我们创建了工艺参数数据库,其中包含全球12种最受欢迎的工业金属的全厚度加工解决方案,以及我们公司著名的解决问题的特殊方法(当金属板材在同一方向上连续出现尺寸偏差时,不要直接重新调整激光参数,而是首先找出其残余应力。
自动化和汽车行业属于高要求领域,我们的控制流程完全满足IATF 16949的要求,并且我们能够提供完整的过程能力分析报告。
<块引用>整个供应链的标准化管控是稳定低废品率的核心支撑。 您可以发送CAD图纸,获得免费的DFM可行性分析,我们将根据废品率控制激光切割标准为您定制定制工艺解决方案,主动降低量产质量风险。
为什么较低的初始单件报价是真正激光切割总成本优化的错觉?
供应商最初提供的单件价格较低,并不意味着采购成本会较低。导致报废、额外校准以及由于装配线停止而导致延误的隐藏问题是激光切割总成本飞速增长的主要原因。
TCO(总拥有成本)生命周期成本细分
当您仅根据每件加工费用做出购买决定时,很多时候您最终会遇到比报价差额高出数倍的隐性损失,这并不代表实际成本优化。我们在内部使用专家激光切割成本分析技术来管理我们的收入和支出并防止任何隐性损失。
我们内部计算单件综合TCO的方法是:单件综合TCO=单件加工费+(单件材料价格废品率)+(每小时生产线停工成本停工时间/批次产量)。该方法是LS Manufacturing专有的会计工具。
- 直接加工成本:它们是供应商报价的单位加工费用,仅占总 TCO 的约 60%-70%。
- 质量损失成本:指的是不合格材料的浪费以及返工的人工和时间成本。
- 供应链延迟成本:它们是装配线停机损失以及由于订单延迟交付而产生的违约成本。
最便宜报价的隐患
最便宜的供应商通常会跳过原材料应力消除、过程取样和正常设备校准等过程,只是确保第一件产品符合尺寸标准。 在批量生产中,公差漂移问题经常发生。 这些供应商通常没有完整的SPC控制系统,无法提供连续的过程能力数据。在客户组装阶段,经常出现批量报废的风险。
激光切割服务真正的TCO优化是工艺单价、量产良率和供应链稳定性之间的权衡,不仅仅是降低初始报价。 本质上,也许每件削减几美元的加工费,最终带来的损失是装配停机和返工量的几倍线。
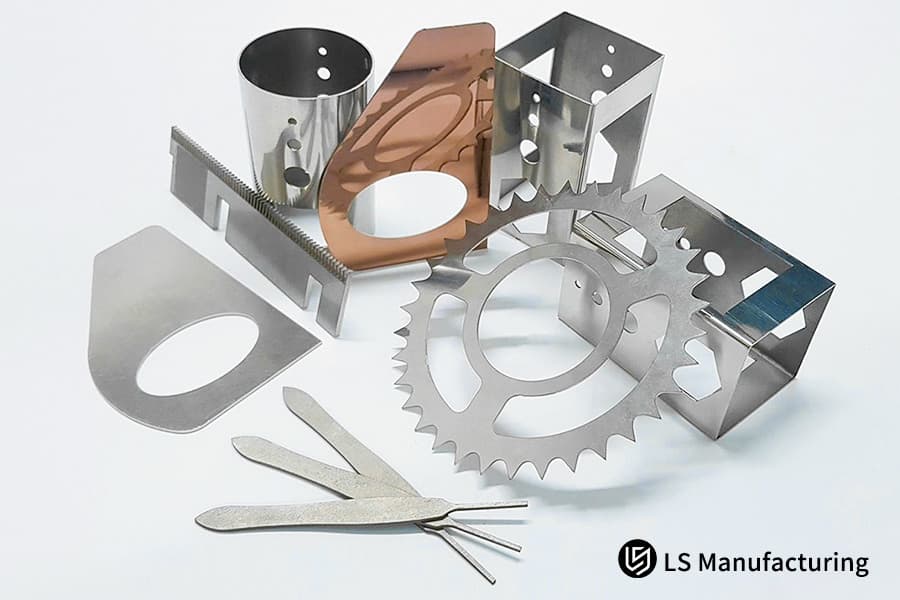
图 1:白色背景上显示各种精密激光切割钢部件。
如何动态调节加工热输入以提供真正精确的激光切割服务?
通过调整激光频率、占空比和喷嘴流体动力学将切缝边缘的热影响区 (HAZ) 宽度控制在 0.1 毫米工业极限以下,这是完全消除激光切割中热偏差的秘诀,从而获得真正可靠的精密激光切割服务。
热变形仿真和多物理场预测
通过多物理场仿真软件,LS Manufacturing的工程师可以预测高能激光释放到薄壁零件上时产生的热变形程度,其激光热源最高温度可达1000°C以上。对于不锈钢、碳钢等各种材料,我们首先依靠专业的激光切割热控制工艺系统,模拟HAZ的扩散范围,提前针对不同切割参数预先优化参数方案。
因此,先进的热控制工艺是制造高质量激光切割零件的关键推动因素。
动态热负荷控制的流程路径
- 微连接优化布局:微米级的微连接可确保零件的位置,从而防止切割过程中因热应力释放而产生位移。
- 多点交错切割路径:跳切轨迹可防止平板因局部热量集中而翘曲。
- 动态氮气比:根据板材厚度实时调节高压辅助氮气流量和压力,非常有效地去除切割区域的热量。
简而言之,这就像不断冷却一个不断升温的部分,同时避免表面达到高温的部分,因此,热变形的可能性较小。
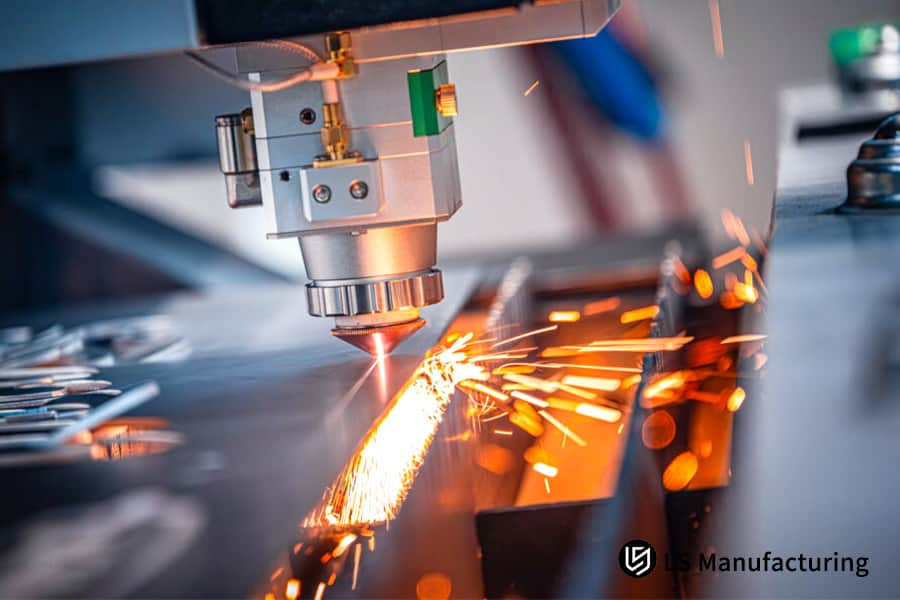
图 2:正在运行的激光切割机正在切割一块金属板,明亮的火花飞舞。
技术参数与费用的矩阵如何证明我们的低废品激光切割服务价值?
使用模糊的形容词无法确定真正的专家。 低废品激光切割服务的真正价值只能通过数字化和匹配在收银线上造成金钱损失的技术参数来揭示。
激光加工解决方案技术与成本对照表
通过多维度的参数比较,遵循标准的激光切割质量审核体系,我们发现高精度解决方案虽然初始成本较高,但考虑到全生命周期成本,结果是相当经济的。
| 评估维度 | 市场标准激光加工 | LS Manufacturing高精度解决方案 | 对 TCO 的影响 |
| 尺寸公差控制 | ±0.15mm,无批次一致性承诺 | ±0.05mm内稳定控制,全批次可追溯。 | 公差偏差直接导致废品和返工成本。 |
| 量产流程Cpk | 无SPC控制,一般在1.0以下 | 稳定≥1.33,关键尺寸可达1.67。 | Cpk越低,批次偏差隐患越高。 |
| 最终装配报废率 | 2%-5% | ≤0.05% | 废品率每增加 1%,总体 TCO 就会增加约 8%。 |
| 原材料应力处理 | 无标准化流程,随机抽样 | 100%精度滚筒调平,逐张验证。 | 残余应力是量产中翘曲偏差的核心原因。 |
| 热影响区 (HAZ) | 宽度≥0.3mm,边缘氧化明显。 | ≤0.08mm,冷切割过程中无明显氧化层。 | HAZ越宽,材料变形和失效的概率就越高。 |
事实上,如果您决定使用LS Manufacturing的激光切割服务,尽管第一个的单价可能会更高,但产生的废料较少。诚然,价格可以降低10%-15%,但当客户考虑到组装阶段发生的报废、返工和劣化损失时,客户的总成本大约下降了25%。
<块引用>参数比较可以清楚地展示解决方案之间的成本差异。您可以提供您现有的采购数据,我们将免费计算您的全周期 TCO 降低量,帮助您根据激光切割服务 TCO 优化标准发现潜在的成本降低量。
图 3:激光切割头聚焦在金属板上,最大限度地减少材料浪费。
为什么严格的原材料应力平衡对于实施废品率控制激光切割至关重要?
冷轧原材料板材时产生的热量使板材产生残余应力分布,是激光切割时残余应力局部释放和板材翘曲的来源。它是批量生产偏差的隐藏因素,是控制激光切割废品率的要素前提。
残余应力偏差机制
毫无疑问,主要用于民用和一般工业用途的冷轧和热轧酸洗板的残余应力不均匀。当零件的长宽比长且宽时,局部热应力和残余应力的结合导致分离部件从零件母材上弯曲,是造成尺寸偏差的直接原因。 激光切割材料校准达到非常精确的水平将可以避免这些变形缺陷。
此外,这一应力控制操作是保证各种高精度定制激光切割部件批量生产的规律性的主要步骤。
不同长宽比零件不平整弯曲程度实测数据
|
比较尺寸 |
市场上的标准激光加工设备 |
LS Manufacturing高精度工业级解决方案 |
|
核心容差稳定性 |
±0.15mm,无批次一致性承诺。 |
±0.05mm内稳定控制,全批次可追溯。 |
|
量产流程Cpk |
无SPC控制,一般在1.0以下 |
稳定≥1.33,关键尺寸可达1.67 |
|
热影响区 (HAZ) |
控制≥0.3mm,边缘氧化明显 |
≤0.08mm,冷切割过程中无明显氧化层 |
|
板材内应力处理流程 |
无标准化处理,随机抽样。 |
100% 精度滚轮调平,每张板材平整度验证。 |
|
装配线末端的总体废品率 |
2%-5% |
≤0.05% |
|
最终 TCO 结果 |
隐性成本高,总体支出超出预期。 |
总体 TCO 降低 25% |
精密滚筒整平工艺效果
- 交替弯曲消除应力:通过使用多组滚轮,使金属板以交替方式反复弯曲,直至完全消除原本因滚压而产生的残余内应力。
- 逐张平整度验证:为了验证板材平整度,每张板材在调平后都会进行测试,以确保整体平整度保持在 0.3 毫米/米以内。
- 防尘防锈存储:平整的板材在恒温恒湿的环境下存储,避免二次变形和表面氧化。
简单来说,就是对板材进行一种“骨骼调整”,即提前释放内应力,防止板材在切割后变形、翘曲。
积极落实Cpk评估标准如何保障激光切割零件制造的稳定性?
通过结合以Cpk(过程能力指数)为重点的统计过程控制,仅在涉及数万件的大生产周期中,件废品率才能始终保持在严格的限度内,从而保证激光切割零件制造。
SPC全流程数据监控系统
为了连续生产数以万计的定制硬件零件,我们依靠数字测量仪器和自动测量站进行定期采样。然后将数据实时输入SPC系统,动态计算实际Cpk值。当数据波动达到预警阈值时,系统通知操作人员进行工艺调整,防止批次缺陷产生,从而全面维护激光切割批次稳定性标准。
这种全流程全数据驱动的管理系统是激光切割废品率控制的主要方法。
批次超差概率对应的Cpk值对照表
|
部分宽高比 |
最大不平整弯曲度 |
行业可接受的阈值 |
|
3:1 |
0.4mm/m |
≤0.5mm/m |
|
6:1 |
0.9mm/m |
≤0.5mm/m |
|
8:1 |
1.5毫米/米 |
≤0.5mm/m |
|
10:1 |
2.1mm/m |
≤0.5mm/m |
Cpk 改进的核心流程控制点
- Laser Nozzle Coaxiality Calibration: The coaxiality deviation between the nozzle and the beam must be controlled within 0.01mm.
- Auxiliary Gas Purity Control: Use 99.999% high-purity nitrogen to avoid gas impurities that may affect the quality of the cutting surface.
- Servo Gap Micron-Level Adjustment: The servo motor feedback gap at the micron level should be controlled to ensure motion positioning accuracy.
Simply put, Cpk is like a "ranking" in the production process, the higher the score, the lower the probability of defective products and the more stable the quality of batch production.
<块引用>Stable process capability is the core guarantee for supply chain security. You can download our Cpk process white paper to gain a deeper understanding of the quality control logic in laser cutting parts manufacturing and assess the quality risks in your current supply chain.
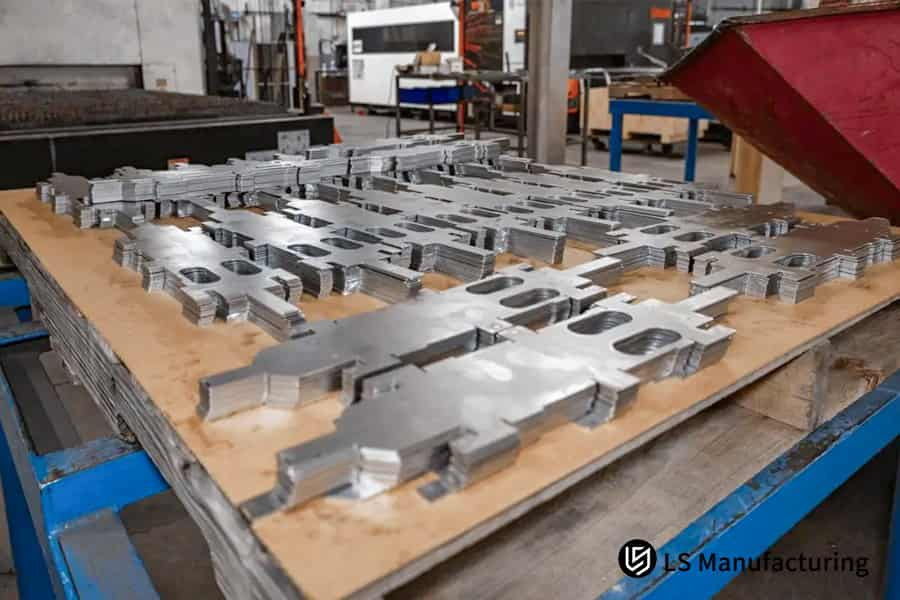
Figure 4: Stacks of laser cut metal parts on a pallet in an industrial facility.
How Do Advanced Nesting Algorithms Reduce Nesting Residual Stress To Keep Custom Laser Cut Components Precise?
Intelligent nesting is not just a matter of enhancing sheet material usage, the primary focus of this method is to minimize the consequences of nesting residual stress via thermal energy loading dispersion treatment. This guarantees the accurate processing result of custom laser cut components.
Thermal Distortion Risks Of Conventional Nesting
Standard nesting simply targets material utilization. At the same time, when parts are closely spaced, heat left over from the cutting of one piece will be directly transmitted to neighboring parts, leading to expansion of the material and dimensions of newly made parts deviating. In addition, deformation of the outer scrap will cause displacement of uncut semi-finished products, because of this increasing tolerances. Dedicated laser cutting thermal nesting algorithms still can effectively resolve this problem.
Using unsuitable nesting methods will drastically cut yield percentages to the point of making it impossible to have stable low-scratch laser cutting production standards.
Key Features of the Thermal Dispersion Nesting Algorithm:
- Cutting Trajectory Alteration: Laser beam hand-off to different parts of the sheet prevents single-spot continuous heating.
- Pre-stiffness Simulation: Determining the stiffness of the skeleton material helps avoid deformation that would cause the shift of semi-finished product.
- Uniform Heat Energy Input: Part laying-out is optimized by heat input uniformity, which in return, leads to heat input balancing and lowering total deformations.
In other words, this is like warming a cake evenly so that it is not burnt in certain spots and the center does not turn out sparse, in which way sheet deformation will be homogeneous.
Based on smart nesting algorithm innovation, one may readily get efficient and low-cost laser cutting service TCO optimization, so harmonizing quality and financial advantages.
Case Study: How Did LS Manufacturing Solve The High TCO Crisis For a Logistics Automation Brand?
One of the famous brands in the logistics automation equipment industry had a big problem when the parts of the chassis of shuttles that were out-of-tolerance were scrapped. We offered a full precision process solution that really worked and through these reduced-scrap laser cutting service, we demonstrated the real value of the solution by A lot reducing their total cost of ownership (TCO).
Customer Dilemma
The customer procured laser-cut chassis core components for the intelligent shuttle vehicle in high-strength steel HC420LA with the requirement that the tolerance was within ±0.06mm. Due to the lack of a mature laser cutting batch optimization solution, the original supplier was not able to control well thermal deformation, and SPC quality control was yet to be developed.
This led to a 4.2% scrap rate in the assembly line as the automatic precision bearing shaft holes often were misaligned causing the assembly line to go through repeated shutdowns and corrections. Based on the customer's calculation, other costs that are caused by a single batch of rework and line downtime are more than $12 000 which further leads to a 35% TCO overrun.
LS 制造解决方案
- Raw Material Pretreatment: The raw sheets of material are passed through a micron-level precision roller leveler that relieves stress and levels the sheets by 100%.
- Process Optimization: We have a self-developed heat load dispersion jump nesting algorithm that is used together with the 99.999% high-purity nitrogen cold cutting process.
- Process Control: We have installed digital display SPC workstations at the key control points for real-time monitoring and quality control of the dimensions.
结果和价值
After the project was implemented, the width of the heat-affected zone at the edge of parts is stably controlled within 0.08mm, and the real-time Cpk is stably maintained at 1.34, fully complying with the process requirements of the IATF 16949 system. The out-of-tolerance scrap rate of those customized core shuttle car components at the assembly line end which was 4.2% dropped to below 0.03% after three consecutive batches totaling over 15,000 pieces, the first-pass yield of assembly line bearings was 99.97%, totally eliminating the customer's secondary manual calibration cost.
In the end, the customer realized a system-level overall TCO reduction of 28% and also LS Manufacturing was recognized as a long-term strategic core supplier by this customer.
<块引用>This mature process solution can be reused for similar precision structural parts. You can send your part drawings to receive a customized quote, and we will tailor a cost-reduction and quality-improvement solution for you based on scrap rate control laser cutting standards, replicating the same quality benefits.

Why Does Strict Regular Optical Maintenance And Alignment Keep Laser Cutting Total Cost From Drifting?
The small thermal lensing or the slight changes in the beam coaxiality of the key optical elements of the laser lead directly to the differences in cutting tolerances in the afternoon versus the morning, and these are also one of the main reasons that indirectly raise the total cost of laser cutting.
The Indirect Cost Consequences of Tolerance Drift
Usually, small processing plants tend to change the lenses only after the parts are visibly deformed and heavily covered with slag. Unfortunately, by that time, hundreds or even thousands of out-of-tolerance scraps would have been delivered to the client. Such kinds of unnoticeable tolerance drifts at the initial piece sampling inspection are almost impossible to detect and typically only become apparent after mass production.
Actually, customers have to deal with rework and downtime losses. Standardized laser cutting optical calibration works as a preventive measure against this hidden threat.
Standardized Optical Maintenance Specifications
- Periodic Beam Inspection: After every 48 hours of continuous operation, employ a beam quality analyzer to examine the laser beam M2 factor and focal space distribution.
- Pre-Shift Coaxiality Verification: Carry out 100% verification of coaxiality and precision nozzle jet flow testing before starting the first shift.
- Regular Consumable Replacement: At fixed time intervals, change protective lenses and focusing lenses to ensure that optical performance degradation does not adversely impact accuracy.
In essence, a regular checkup of the laser equipment is like a "health maintenance plan" during which small problems can be spotted early and major malfunctions that lead to downtime and scrap can be avoided.
<块引用>Standardized equipment maintenance is the foundation for stable batch accuracy. You can contact our engineering team for a one-on-one consultation to learn about our end-to-end accuracy assurance solutions for custom laser cut components, tailored to your mass production needs.
Why Do Global Engineering Buyers Rely On Our Premium Laser Cutting Service For Long-Term Supply Stability?
In the field of mass production of industrial components, having a skilled manufacturing partner who understands how to convert engineering ideas into real assembly advantages and supply chain security is very important. The decision to select a dependable laser cutting service is crucial for securing supply stability over the long term.
Our complete set of engineering skills and an extensive quality system are the main factors why worldwide engineering purchasers keep us in mind as a long-term partner.
In Humen Dongguan LS Manufacturing continues to exploit its well established industrial support advantages to provide clients with prototyping and mass production solutions promptly. After getting familiar with IATF 16949 and ISO 9001 standards, we have set up a full-fledged quality management system. With the launch of a thorough laser cutting supply assurance system, we are in a position to offer our customers a complimentary DFM (Design for Manufacturing) feasibility evaluation while still at the prototyping phase.
Opting for us means that, besides metal parts, clients receive system-level quality assurance for automated production lines that operate with zero tolerance, zero delays, and zero rework, so completely eliminating supply chain quality risks.
FAQs
Q1: How do you identify whether a laser cutting quote includes comprehensive TCO optimization?
One way of knowing if the laser cutting quote is truly optimized for the total cost of ownership (TCO) is that it not only mentions the base machine time charge but also explicitly lists the costs of material de-stress and leveling, the heat-affected zone control parameters, the ratio of full inspection sampling, and the Cpk stability guarantee covering all the lifecycle cost elements.
Q2: What physically parameters set the off-die scrap rate during continuous laser processing?
The key parameters include the M2 factor of the beam (controlled within 1.1), the nitrogen pressure of the nozzle (1.2-1.5MPa), and whether the width of the edge heat affected zone is strictly limited to below 0.1mm, which directly determines the level of scrap rate.
Q3: Will LS Manufacturing be able to achieve the tolerances on laser parts within plus or minus ±0.05 mm?
This relates to the quantity of high volume carbon steel orders.Yes, by importing high precision high power fiber laser machine and adopting dynamic kerf compensation algorithm and real time SPC monitor, we can keep the accuracy tolerance in tolerance control requirement of ±0.05mm for mass production.
Q4: Why does material thickness simultaneously affect the total cost and tolerance performance of laser cutting?
Beyond Really the thicker the sheet metal is, the bigger the laser power and gas consumption are, leading to a significant increase in heat input, more sophisticated jump-patterning algorithms must be used so that thermal distortion does not exceed tolerances, this way raising the costs of processing and control.
Q5: How does your low-scratching laser cutting service help clients avoid costly assembly line downtime?
We keep production tolerances very tight so that the parts that go to the customers' production lines can be assembled 100% smoothly without any problem. This way, there is no risk that the automated assembly lines will be stopped because of dimension errors.
Q6: What kind of certificates should a top-quality laser parts manufacturer for B2B have to show that they meet industrial standards?
At a minimum, they should be certified for ISO 9001 system. If they deliver specially tailored components to specific industries having high demands, then strictly following IATF 16949 or the appropriate industry Cpk process specifications is needed for production control.
Q7: How are micro-joints in high-tech nesting helpful in saving manufacturing costs while still ensuring the parts are highly precise?
Micro-joints arranged at micron level, if done properly, prevent the thin and small parts from being displaced and deflecting during cutting by the high-pressure gas blowing. So, this leads to very high precision and the parts won't warp or clash. This way, possibility of scrap is very low.
Q8: What is the minimum order quantity (MOQ) for a precision laser cutting service which leads to an explicitly optimized TCO?
When it comes to the high-precision orders which require thorough SPC management and complete stress relief, 500 pieces is the most economical production starting point we can recommend. This batch size offers excellent per-piece TCO cost savings. You can even upload your drawings directly to us to get the exact quote.
Summary
Controlling the total cost of ownership (TCO) for laser-cut parts of large-volume remains a complex and long-term commitment to an efficient and integrated engineering system that identifies all causes of raw material stress, uses methods of thermal distortion reduction during operations and continuously monitors dynamic Cpk data throughout the whole process. Suppliers simply offering a low price and no technological and quality management skills, usually make parts with an internal 2%-5% scrap rate, ultimately causing great delays and losses to buyers in the supply chain.
You should not cover the high rework costs for parts out of tolerance at the assembly line level. LS Manufacturing is a very experienced Industrial manufacturer established in high-precision manufacturing region of China. The company has equipped itself with very high-power industrial fiber laser cutting clusters and a full set of precision roller stress-relieving and leveling equipment. The entire industrial customization project team of LS Manufacturing is entirely capable of compromising between low scrapping rate and high Cpk stability and process capability, so providing with system-level TCO locked from the source.
We would be glad if you can contact our expert team immediately and send your 2D/3D CAD drawings (supporting STEP/DXF formats) to our official email address. Within 24 hours, we shall return a professional and in-depth technical quotation to you with process feasibility analysis and thermal deformation prevention strategies that will help you embark on a real cost-lean transformation.
📞Tel: +86 185 6675 9667
📧Email: info@lsrpf.com
🌐Website: https://lsrpf.com/
Disclaimer
The contents of this page are for informational purposes only. LS Manufacturing services There are no representations or warranties, express or implied, as to the accuracy, completeness or validity of the information. It should not be inferred that a third-party supplier or manufacturer will provide performance parameters, geometric tolerances, specific design characteristics, material quality and type or workmanship through the LS Manufacturing network. It's the buyer's responsibility. Require parts quotation Identify specific requirements for these sections.Please contact us for more information.
LS Manufacturing Team
LS Manufacturing is an industry-leading company. Focus on custom manufacturing solutions. We have over 20 years of experience with over 5,000 customers, and we focus on high precision CNC machining, Sheet metal manufacturing, 3D printing, Injection molding. Metal stamping,and other one-stop manufacturing services.
Our factory is equipped with over 100 state-of-the-art 5-axis machining centers, ISO 9001:2015 certified. We provide fast, efficient and high-quality manufacturing solutions to customers in more than 150 countries around the world. Whether it is small volume production or large-scale customization, we can meet your needs with the fastest delivery within 24 hours. choose LS Manufacturing. This means selection efficiency, quality and professionalism.
To learn more, visit our website:www.lsrpf.com.


|
Cpk 值 |
每百万单位中超出公差的数量 |
量产稳定性水平 |
|
1.0 |
2700 单位 |
基本可以接受 |
|
1.33 |
63 单位 |
稳定级别 |
|
1.67 |
0.6 单位 |
优秀级别 |
|
2.0 |
0.002 单位 |
终极级别 |
